How do resin 3D printing technologies like SLA and DLP work?
How do resin 3D printing technologies like SLA and DLP work?
SLA and DLP both cure liquid photopolymer layer by layer, but they expose the material differently. Spot or pixel size, layer thickness, exposure, orientation, support strategy, and post-cure affect the final result.
What is the process difference?
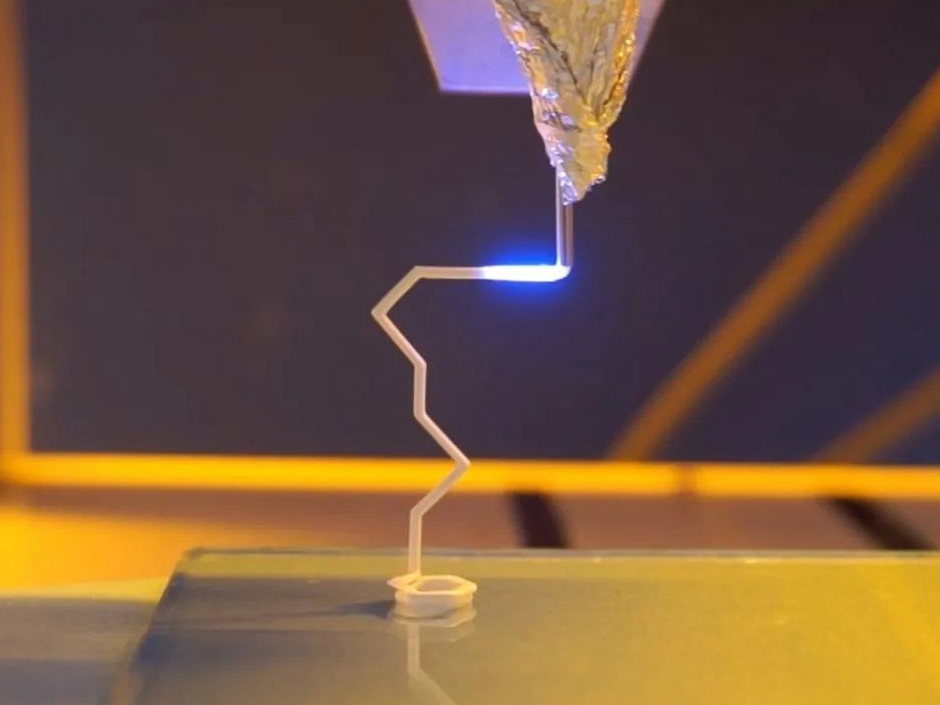
SLA traces or exposes a region with a laser, while DLP projects an image for a layer. DLP can expose many pixels at once, while SLA may offer a different feature and build tradeoff. Machine and resin qualification matter more than the label alone.
A related process may use different exposure or peeling conditions; ask for the actual machine, resin, layer, and cure procedure.
What does orientation change?
Orientation changes support contact, peel force, suction, exposure history, and the direction in which a thin feature is measured. A detail-friendly orientation may create marks or trapped resin elsewhere. Choose orientation with the critical feature and cleaning path in view, then verify the final cured mating surface rather than the as-printed surface.
Orientation changes support marks, peel forces, suction, anisotropy, dimensional compensation, and which face receives the best detail. A detailed face may need support-free placement or a controlled finishing allowance.
Blind cavities need drainage and cleaning access. Trapped resin is a functional defect, not a cosmetic issue.
How should a buyer choose?
Choose by feature, quantity, surface, material state, and required evidence. SLA guidance and DLP guidance are starting points; the quote must define the final cured part.
SLA and DLP differ in how each layer is exposed, but machine settings and resin response can matter more than the acronym. Pixel or spot size, layer thickness, exposure compensation, peel force, orientation, and supports affect dimensional results. Ask for the actual machine, resin, layer, exposure, wash, and cure route when a feature is critical.
Orientation is a compromise. A face placed for detail may need supports or may experience peel stress. A long hollow section may need drainage. A large flat area may curl or create suction. A production-ready orientation balances detail, support contact, dimensional stability, cleaning, and build time.
The measurement state is after washing, drying, and post-curing. Compare the same state when checking tolerance, because cure can change dimensions and stiffness. If finishing is allowed, state how much material may be removed and which datum must remain untouched.
A useful first article records the orientation, support strategy, resin lot, layer, cure schedule, and final measurements. That record makes the chosen technology reproducible instead of treating a successful sample as a permanent guarantee.
SLA and DLP selection should also consider build height, support, peel force, cavity drainage, and the resin's intended use. A process that produces a sharp outside edge may still trap resin inside a hollow part.
Request a first article with the same orientation and cure route expected in production.
SLA and DLP should be selected with drainage, supports, peel forces, and cure in mind. A nominal resolution cannot predict a cavity's cleanliness or a thin wall's service life. The first article should represent the planned orientation and final process.
SLA and DLP should be compared by exposure, layer, support, peel, drainage, cure, and final geometry. A sharp outside edge does not prove a cavity is clean. Ask for the actual machine and resin route when a small feature or thin wall controls the purchase.
The first article should use the planned orientation and support strategy, then record resin lot, cure, dimensions, and surface.
SLA and DLP route selection should include build height, exposure, layer, support, peel, drainage, wash, and cure. A face may need supports to preserve detail, while a cavity may need a drain path to prevent uncured resin. Large flat sections may create suction or distortion. Ask for the planned orientation and for a first article made with the same resin and cure route.
The first-article record should include resin lot, machine, layer, support strategy, wash, cure, dimensions, and surface condition. This makes later batches comparable.
The process review should include cavity drainage and the ability to confirm that uncured resin has been removed. A hollow body can look correct while retaining liquid material. Ask for the wash, dry, cure, and residue method and for a final inspection that reaches the inside when the cavity matters.
A detail-driven order should identify the feature, datum, tolerance, surface, and final cure. If the use is visual, classify the part as a model. If the use is functional, add the relevant heat, UV, chemical, load, or cycle condition. This simple classification prevents a fine-feature result from being mistaken for a service-life result and tells the supplier what evidence belongs in the quote.
The final inspection should be performed after all required cure and finishing steps, because support removal and sanding can change the feature that made resin attractive. Record the final surface and the mating condition when the part is accepted. Include the measurement condition and tolerance basis.
The detail requirement should be checked after the complete cure and finish sequence.
Technology selection and first article
SLA traces or exposes a region with a laser, while DLP projects an image across a layer. Pixel or spot size, layer thickness, exposure compensation, peel force, orientation, and support strategy affect the finished feature. The acronym is therefore insufficient for selecting a critical part. resin materials
For a thin wall or mating surface, choose orientation with support marks, suction, drainage, and measurement access in view. Inspect after washing, drying, and post-curing, not in the liquid or partially cured state. can frame the resin route and vat photopolymerization the relevant material treatment, but the first article should record machine, resin lot, exposure, wash, cure, critical feature, and acceptance test.