What Are The 3D Printing Technologies Used for Resin Parts Additive Manufacturing?
 Resin additive manufacturing is a route-selection and material-state decision, not a promise that every photopolymer part is dimensionally stable or production-ready. For a detail-critical prototype, screen SLA or DLP; for a multi-material visual study, screen PolyJet; for a repeated batch, screen CLIP, provided the final cure and acceptance test are specified. SLA, DLP, CLIP, and PolyJet all cure or deposit a light-reactive resin, but they differ in how energy reaches the material, how support is removed, how the part is post-cured, and how the material ages. Choose the process against feature size, quantity, surface, toughness, temperature, transparency, flexibility, or castability, provided that the final cure state, environment, and acceptance method are defined before the build is released. The resin 3D printing service should be quoted with the material family, cure condition, finishing route, and acceptance test attached.
Resin Process and Final State
Photopolymer resin starts as a liquid formulation containing reactive oligomers, monomers, photoinitiators, pigments, and sometimes fillers. Exposure to the selected wavelength initiates polymerization. Conversion is not identical to a finished engineering property: exposure dose, layer thickness, vat temperature, oxygen inhibition, support contact, washing, drying, and post-cure affect the network that remains. The same nominal “tough” or “high-temperature” label can therefore produce a different result when the supplier changes the formulation or the cure schedule.
Define the delivered state before comparing machines. A part may be as-printed, washed and dried, UV post-cured, thermally post-cured, painted, machined, or assembled with inserts. Record the resin product and lot, exposure or build profile, cleaning solvent and time, post-cure wavelength, intensity, time, temperature, and storage interval. Dimensional inspection and mechanical testing must use that final state. A green or insufficiently cured part is not evidence for the service condition, and a fully cured part is not automatically resistant to heat, chemicals, impact, or long-term UV exposure.
SLA Laser Curing
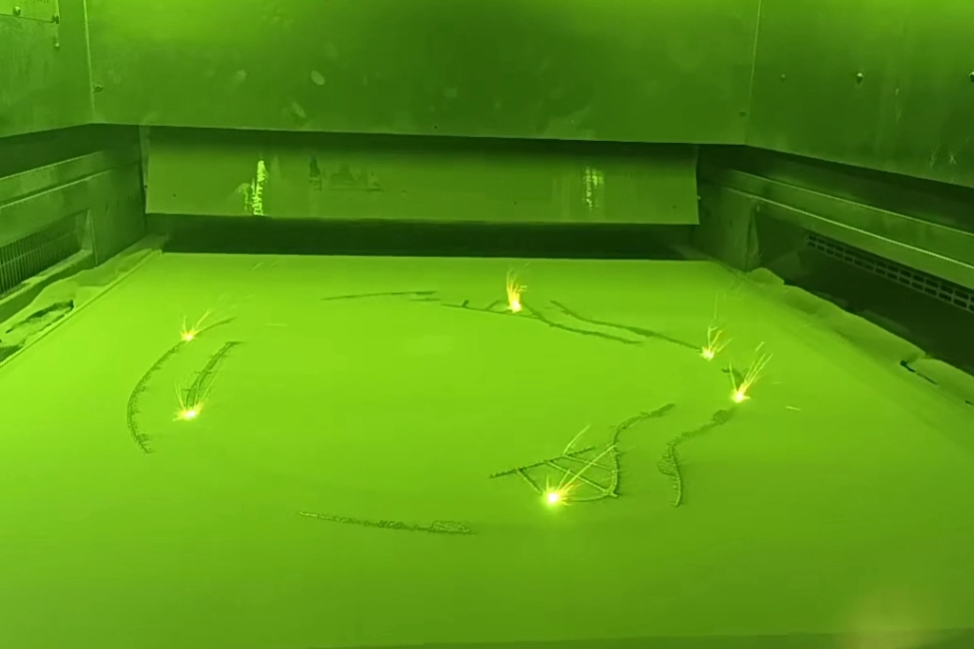
Stereolithography, or SLA, uses a laser to trace the cross-section of each layer in a vat of photopolymer. The laser spot, scan strategy, resin viscosity, exposure dose, layer thickness, and recoating behavior influence edge definition and cure depth. Fine layers can reduce visible stair stepping, but they do not remove shrinkage, optical bleed, support marks, or anisotropy. A quoted layer height is a machine setting; it is not a tolerance for every wall, hole, orientation, or resin until the specified final condition is measured.
SLA is often screened for visual prototypes, housings, masters, casting patterns, dental models, and detail-critical low-volume parts. Standard resin is useful for form and fit when the load is modest. Tough resin can be considered for clips or functional prototypes, but impact performance depends on section thickness, notch geometry, orientation, and post-cure. Castable resin is selected for an investment-casting workflow and must be validated for burnout residue and shell compatibility. High-temperature resin needs a defined temperature-time condition; a catalog heat-deflection value does not mean continuous service at that temperature.
DLP: Pixel Exposure and Cure Window
Digital Light Processing, or DLP, projects a complete layer through a pixelated imaging system. Because many pixels are exposed at once, production time can be less sensitive to the number of parts within the projected field than SLA scanning time. Pixel size and optical calibration influence the smallest reliable feature, while exposure time, light intensity, resin absorption, and overcure influence dimensional fidelity. Curved edges can show pixel stepping, and a small nominal pixel does not guarantee a small hole or a sharp internal corner.
DLP is a practical candidate for dental models, jewelry patterns, small functional batches, and repeat parts that fit the build area. A buyer should compare exposure uniformity, build-area position, support strategy, and post-cure capability rather than compare “speed” alone. For a thin-walled electronics prototype, inspect wall thickness and snap-fit deflection after the agreed cure. For a pattern used in casting, inspect burnout behavior and dimensional change after the complete pattern-to-casting workflow. Vat photopolymerization is a useful process family reference, but the selected resin and final-state process still govern the result when measured in the delivered condition.
PolyJet: Multi-Material Deposition
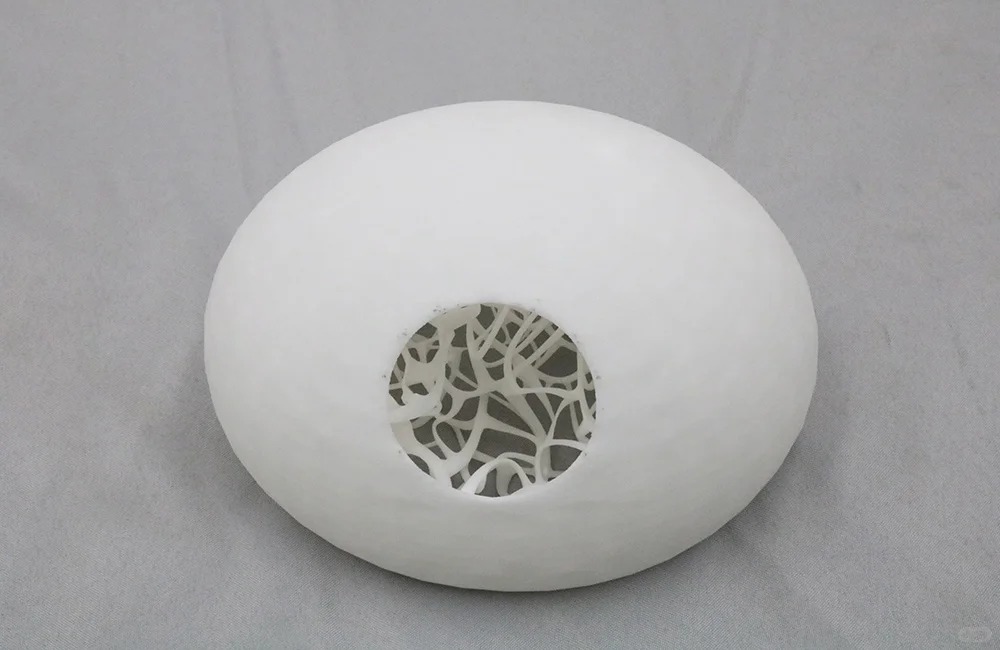
PolyJet jets small droplets of photopolymer and support material onto a build surface, then cures the deposited material with light. It can place rigid, rubber-like, transparent, or colored formulations in one build when the platform and material combination is qualified for that use. The mechanism is different from vat curing: droplet placement, layer leveling, support removal, material interfaces, and local cure history influence the part. A multi-material assembly is not equivalent to a bonded production component because the interface can have different stiffness, swelling, or aging behavior.
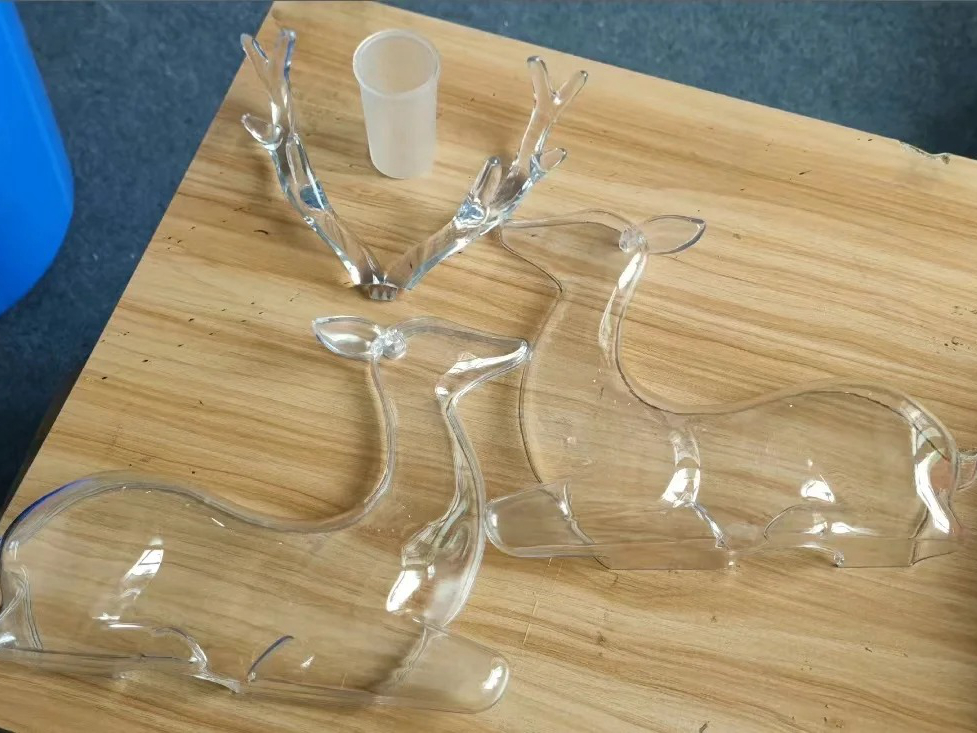
PolyJet is valuable for a form-and-feel prototype, a transparent visual model, a soft-touch overmold study, or a small multi-material ergonomic sample. Use material jetting when the buyer needs those capabilities and can accept the material's service limits. Transparent parts may require polishing and still show internal haze or directional artifacts. Flexible regions can creep, tear, or change hardness after solvent exposure and humidity. If the prototype is used for a load or sealing test, specify the strain, dwell, temperature, fluid, and number of cycles; do not infer production elastomer life from a short demonstration.
CLIP: Continuous Production Window
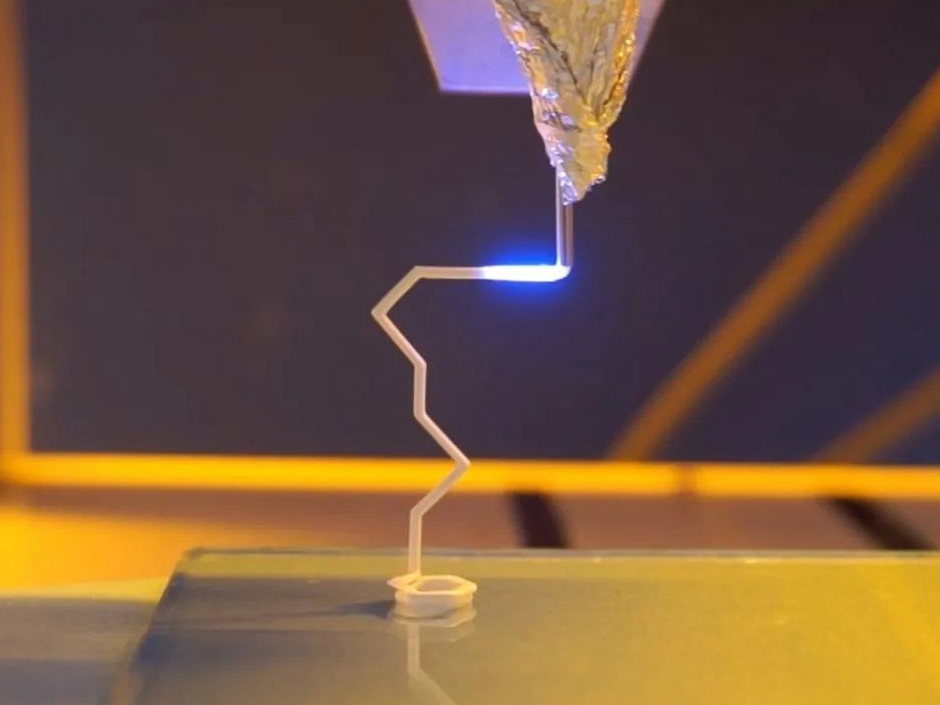
Continuous Liquid Interface Production, or CLIP, uses projected UV light and an oxygen-inhibited region near a permeable window to keep a controlled “dead zone” between the window and the growing part. The resin rises continuously while the platform moves, reducing the stop-and-start layer separation used in conventional vat processes when the qualified build profile permits it. The benefit is a different thermal, exposure, and separation history, not a universal speed multiplier. Build height, cross-sectional area, resin rheology, support design, cooling, and post-cure determine the delivered cycle time and properties.
CLIP can be considered for repeated engineering prototypes or production-like batches when a compatible durable, tough, or high-temperature resin has a validated cure and conditioning route. A large solid cross-section may still require slower settings or thermal management. Thin features may be limited by wash access, support removal, and the resin's cured brittleness. When comparing CLIP with SLA or DLP, measure accepted parts per batch, support and finishing labor, dimensional yield, and the final functional test. A build that finishes sooner is not lower cost if overcure, warpage, failed supports, or post-cure variation creates rework.
Resin Material Families and Limits
Material family | Useful screening case | Main condition to control | Evidence before release |
|---|---|---|---|
Standard resin | Visual, form, and fit prototypes | Brittleness, cure shrinkage, and surface handling | Dimensions, surface, fit, and short functional check |
Tough or durable resin | Clips, housings, and low-load functional prototypes | Section thickness, notch sensitivity, orientation, and aging | Deflection or impact test in the final cure state |
High-temperature resin | Short-duration thermal fixtures or heat exposure studies | Time at temperature, load, post-cure, and thermal cycling | Thermal exposure with dimensions and load function measured |
Flexible resin | Seals, grips, and ergonomic samples | Hardness drift, tear, creep, solvent, and humidity | Compression, tensile, tear, and environmental conditioning |
Castable resin | Patterns for investment or lost-wax casting | Burnout schedule, ash, shell compatibility, and shrinkage | Pattern measurement and representative casting inspection |
Transparent or dental resin | Optical models or device-specific prototypes | Optical path, biocompatibility scope, cure, and cleaning | Visual or optical test and application-specific documentation |
Material names must remain tied to a supplier formulation and condition. Standard, tough, high-temperature, castable, flexible, transparent, and medical or dental resins are not interchangeable categories for a safety decision. A high-temperature resin can retain shape for a short unreinforced fixture exposure and still fail under sustained load or repeated thermal cycling. A resin with patient-contact documentation may be suitable only for a named device type, contact duration, cleaning method, and validated post-cure. The resin material range should be narrowed by the use case before a quote is compared.
Process Comparison and Buyer Route
Route | Choose it first when | Typical trade-off | Key acceptance evidence |
|---|---|---|---|
SLA | Fine detail, smooth masters, or a broad low-volume part envelope | Laser time, supports, cure shrinkage, and anisotropic behavior | Feature dimensions, fit, surface, and final-cure test |
DLP | Small repeat parts or patterns that fit a calibrated projection field | Pixel artifacts, field uniformity, and exposure overcure | Position-based dimensional map and functional samples |
PolyJet | Multi-material, color, texture, or soft-touch prototypes | Material interfaces, solvent sensitivity, and long-term aging | Interface, hardness, deformation, and environmental checks |
CLIP | Repeated builds where throughput and engineering resin performance are both needed | Resin-specific process window, support labor, and thermal management | Batch yield, dimensions, cure state, and functional test |
For a consumer-electronics enclosure with a snap fit, SLA or DLP may be screened for detail; select a tough resin only if its deflection, retention force, and aging are tested in the final cure state. For a medical planning model, choose DLP when small repeatable features and a verified deviation map matter; select PolyJet when color, texture, or flexible regions are part of the planning review, provided the cleaning and contact scope are documented. For a dental or surgical model, DLP or PolyJet may fit the geometry and workflow, but model material, patient-contact material, and sterilizable device material must be separated. For a casting pattern, SLA or DLP with castable resin may be preferable to a tough resin because burnout behavior matters more than impact resistance. For a small batch of multi-material ergonomic housings, PolyJet may save assembly time, while a production claim still needs separate validation.
Cost and quantity should be compared using resin consumption, build occupancy, machine time, supports, washing, post-cure, finishing, failed-part allowance, inspection, packaging, and rework. A single detailed prototype can favor SLA; a repeat field of identical parts can favor DLP or CLIP if yield and cure consistency are known. PolyJet can be economical for one integrated multi-material prototype even when it is not the lowest unit cost for a single rigid part. Ask for accepted-part yield and finishing labor, not only the advertised print rate.
Failure Modes and Verification
Under-cure can leave low conversion, tackiness, weak interlayer bonding, and unstable dimensions. When producing a releasable part, control resin age, vat condition, exposure profile, wash time, drying, and post-cure; then measure hardness or mechanical response in the delivered state. Over-cure and optical bleed can close holes, thicken thin walls, and reduce channel clearance. Use a feature coupon or a geometry-representative sample to map the condition instead of converting a nominal pixel or laser spot size into a drawing tolerance.
Resin parts can warp during support removal or post-cure because shrinkage is constrained by geometry and the cure gradient. Control orientation, support contact, wall thickness, drainage, and cure fixture; inspect datums after the complete finishing sequence. UV, heat, humidity, solvents, and repeated loading can embrittle, swell, soften, or discolor a photopolymer. Define exposure duration, temperature, fluid, load, and cycle count, then compare the measured change with the project criterion. Surface treatment can improve appearance or protect a surface, but it cannot restore an under-cured core or prove chemical compatibility; use the surface-treatment route only after the base part passes its own checks.
Use a named standard only when the method and acceptance authority accept it. ASTM D638 may be considered for tensile testing of suitable plastic specimens, ASTM D2240 for hardness, and ASTM D543 for chemical resistance screening, but a standard coupon is not a release test for every photopolymer geometry. Record the resin product and lot, build orientation, cure state, specimen location, conditioning, test temperature, measurement uncertainty, and acceptance criterion. If medical, dental, food-contact, or skin-contact use is proposed, require the applicable formulation documentation and device-level validation; resin printing alone does not establish biocompatibility or regulatory approval.
RFQ and Release Path
Provide the CAD and drawing revision, part quantity, critical dimensions, minimum wall and hole sizes, surface requirement, material family or approved resin, temperature and chemical exposure, load or deflection, transparency or flexibility need, casting or medical boundary, color, support-mark allowance, and required final state. Identify whether the request is visual, form-and-fit, functional prototype, casting pattern, dental model, device-development sample, or repeat production-like batch. The supplier can then compare SLA, DLP, CLIP, and PolyJet against the actual geometry and risk.
Before release, request the resin product and lot record, machine and build record, washing and post-cure record, dimensional report, surface or visual inspection, and functional or environmental test data where required. Define which deviations require rework, a repeat measurement, engineering review, or rejection. Resin additive manufacturing is effective when the process, formulation, final cure state, environment, and acceptance method are treated as one controlled system.
FAQs
Which 3D printing technology is best for producing high-precision resin parts?
What are the most commonly used resin materials in PolyJet printing?
How does Continuous Liquid Interface Production (CLIP) improve production speed for resin parts?
Can SLA be used for producing high-strength resin parts, and what are its advantages?
What are the key benefits of using resin-based 3D printing in the medical industry?