Which industries benefit the most from stainless steel 3D printing?
Which industries benefit the most from stainless steel 3D printing?
Aerospace, automotive, medical, tooling, energy, and industrial equipment can all benefit, but the useful application is defined by the duty and evidence requirement rather than by the industry label. A part should be screened for corrosion, temperature, load, geometry, cleanliness, quantity, and the consequences of failure before the grade or process is selected.
Which applications are good candidates?
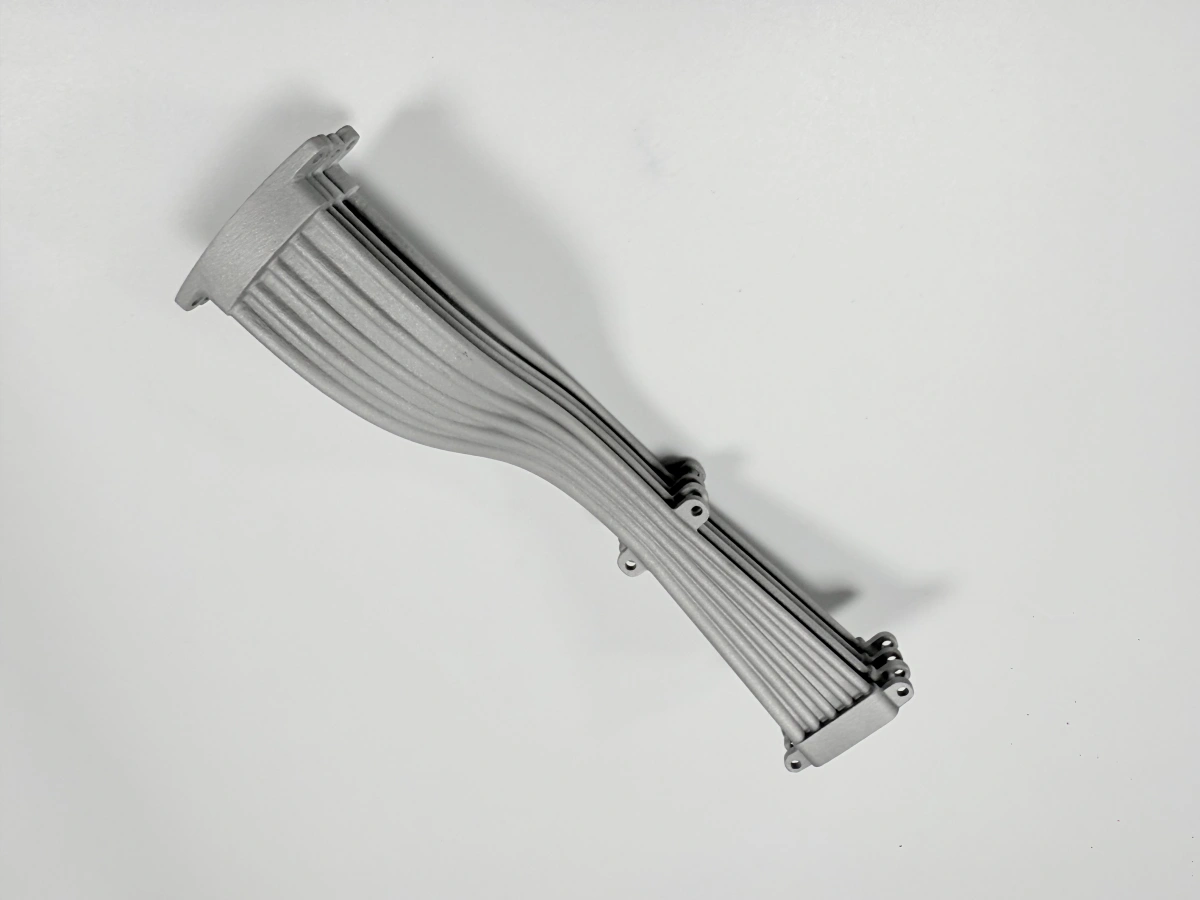
A manifold is a good candidate when the printed passage removes brazed joints and the buyer can specify cleaning and leak testing. A simple bracket is a candidate only when the build direction, machined hole, and fatigue load are controlled. The application decision therefore depends on the feature that fails first, not on the industry label.
Good candidates include low-volume brackets, fixtures, conformal cooling inserts, corrosion-resistant manifolds, and replacement parts with complex or discontinued geometry. The common feature is a business or engineering constraint that conventional production handles poorly.
For aerospace and aviation, qualification and traceability can dominate the decision. For medical and healthcare, cleaning, material identity, and regulatory scope must be defined. For tooling, wear, thermal cycling, and the repair or replacement path usually matter more than headline tensile strength.
Which applications need caution?
A part exposed to an aggressive chemical, a pressure boundary, a fatigue load, or a regulated biological environment needs a project-specific acceptance plan. The word stainless does not guarantee corrosion resistance in every medium, and a printed density claim does not prove leak tightness.
Thin unsupported sections, enclosed powder, inaccessible surfaces, and a required mirror finish may also make the route impractical. Redesign, hybrid machining, or a conventional process may be better if the additive geometry does not solve a real constraint.
What evidence should be requested?
Request the named grade and lot, build record, heat-treatment or stress-relief record, dimensional report, surface condition, and any agreed density, CT, metallography, pressure, or load test. The acceptance method should identify the feature and failure mode it controls.
The RFQ should also name whether the part is a prototype or a production item, the inspection authority, and the final state for measurement. This prevents a general industry example from being mistaken for a qualification package.
Aerospace and aviation parts normally carry the highest traceability burden. The buyer must separate a concept model, a ground-support item, a non-flight functional article, and a flight-qualified component. The same stainless grade and printer can appear in all four categories, but the required material control, process qualification, inspection, and approval are different. Ask the supplier to state which records are standard and which require a project-specific qualification plan.
Automotive applications often justify printing through lightweighting, consolidated ducts, fixtures, or a fast replacement rather than through a universal material advantage. The part may see vibration, thermal cycling, road chemicals, or repeated assembly. A bracket that passes a static pull test can still fail at a rough support-marked surface under vibration. Define cycles, attachment torque, temperature, and inspection locations when those conditions control the use.
Medical and healthcare applications add cleaning, surface, traceability, and regulatory questions. “Stainless steel” does not by itself establish suitability for an implant, an instrument, or a non-contact fixture. State the intended contact, cleaning or sterilization, corrosion environment, and responsible approval owner. For tooling and industrial equipment, wear, repair access, and repeatable fit may matter more than the highest tensile number. Each industry needs its own evidence branch.
A good screening meeting asks four questions. What failure ends the part's useful life? Can the printed geometry be cleaned and inspected? Which final state is being purchased? What test will make the release decision? If the answer is vague, redesign or a conventional route may be preferable. If the answers are specific, the supplier can select a route and return a quote with assumptions rather than a generic promise.
For a regulated or safety-related application, the industry name does not replace qualification. Define the approval owner, traceability depth, cleaning or sterilization, and the consequence of failure. For a general industrial part, the evidence may be lighter, but the failure mode still has to be named.
A buyer should ask for a sample report before placing a batch order. That reveals whether the supplier can report the property in the requested condition and whether the proposed inspection actually reaches the critical feature.
Industry selection should also include supply and approval risk. Ask whether the supplier can maintain the grade and final condition over repeat orders, whether the part can be cleaned and inspected, and whether the records meet the responsible organization's needs. A small industrial fixture may need only dimensional and functional evidence; a flight or medical application may need a much deeper qualification path.
Industry fit also depends on what is allowed to be changed. An automotive prototype may accept a material or finish change during development, while a medical or aerospace part may require locked material and process records. A tooling component may be accepted through a production trial, while a pressure part needs a defined leak criterion. Identify the approval path before selecting the process.
A buyer should ask for a sample report and a list of exclusions. This reveals whether the supplier is quoting a prototype, a functional non-regulated component, or a qualified production part. The same stainless grade can appear in all three categories without carrying the same evidence.
Industry-specific qualification boundary
Industry labels are only a screening start. An aerospace bracket needs traceability, orientation-aware mechanical evidence, and dimensional control at the machined attachment points. A tooling insert needs thermal-cycle and wear evidence at the working surface. A medical non-contact fit-check needs cleaning and dimensional evidence, while a patient-contact claim requires a separate regulatory qualification. These are different decisions even when the same stainless powder is used. stainless heat treatment
For a pressure or fluid application, the qualification boundary is the delivered passage and its connection, not the industry name. Review the route with the grade, service medium, temperature, and inspection access defined. If a heat-treatment record is required, metal powder-bed fusion should identify the alloy condition and measurement state. Any deviation should have a named disposition owner before the part is accepted.
.webp)