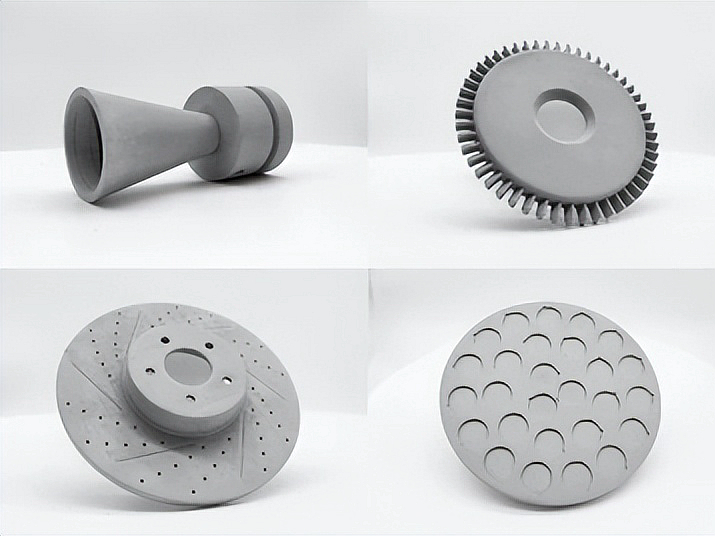
What are the most common 3D printing technologies for ceramics?
What are the most common 3D printing technologies for ceramics?
The common ceramic 3D printing routes are ceramic SLA or DLP, binder jetting, and material extrusion; specialized material-jetting and powder routes may be available for supplier-qualified applications. Each route creates a different green body and therefore a different debinding, sintering, or firing risk. Alumina, zirconia, silica, silicon nitride, and silicon carbide need route-specific feedstock, solids loading, thermal profile, shrinkage, density, and inspection evidence. Choose a technology from detail, size, quantity, surface, material, and the final fired condition.
Ceramic SLA and DLP
The mechanism of ceramic SLA and DLP is light curing of a photosensitive slurry containing ceramic particles. Layer exposure, slurry viscosity, particle loading, sedimentation, cure depth, support, and washing govern the green body because they change particle distribution and cured-binder strength. Debinding then removes the organic phase before sintering develops the ceramic density and dimensions. This route can suit fine features and small technical geometries, but a high-resolution green shape does not ensure a fired part without a verified crack assessment. For a zirconia dental or technical form, choose SLA/DLP only when cure, debinding, firing, shrinkage, and surface are qualified; verify phase, density, dimensions, and final function.
Binder Jetting
The mechanism of binder jetting is selective liquid-binder deposition into a ceramic powder bed. Powder size distribution, packing, binder saturation, layer thickness, green-body strength, and powder removal control the unfired part because they determine local support and permeability; retain that control only when the powder lot and packing condition are recorded. Debinding and sintering determine shrinkage, density, porosity, and warpage. Binder jetting can suit selected batch geometries, but delicate green parts require controlled handling and furnace support. For an alumina or silicon carbide batch component, choose binder jetting only when powder, binder, debinding, firing atmosphere, and dimensional compensation are validated; verify density, porosity, dimensions, fracture-sensitive surfaces, and functional performance.
Material Extrusion
Material extrusion deposits ceramic-filled filament, paste, or another bead-like feedstock. Nozzle size, viscosity, bead width, layer bonding, drying, moisture, support, and path direction influence green-body anisotropy. It can be useful for larger or simpler forms, prototypes, architectural or artistic work, and selected technical geometries. The fired part may retain a directional shrinkage or surface texture. For a silicon nitride fixture or silica design object, choose extrusion when size and feedstock behavior fit the project; verify drying, debinding, firing, fired dimensions, density, and surface acceptance.
Specialized Routes and Material Jetting
Material jetting and laser powder-bed approaches for ceramics are not one universal category. A supplier may use a specialized binder or particle-loaded feedstock for patterns, research, or a defined fired product. High thermal gradients and ceramic brittleness can make laser fusion difficult, while a printed polymer or binder pattern is not itself a finished ceramic. Ask what material conversion follows deposition. For a silicon carbide or alumina research component, select a specialized route only when final composition, debinding or firing, density, porosity, and thermal or mechanical evidence are available.
Route Choice and RFQ
Compare SLA, DLP, binder jetting, material extrusion, and specialized routes using detail, size, quantity, support, green-body handling, shrinkage, density, porosity, surface, inspection, and post-processing. A route with fine resolution can still fail if the fired channel cannot be cleaned or measured. A batch route can still be unsuitable if density varies across the furnace load. Include vat photopolymerization, binder jetting, and material extrusion as complete process chains.
For an RFQ, provide ceramic grade, feedstock and lot, route, CAD and drawing revision, quantity, green-body support, shrinkage allowance, fired dimensions, density, porosity, load, temperature, atmosphere, fluid, pressure, surface, cleaning or sterilization, inspection access, schedule, and approval authority. Request print, drying, debinding, sintering or firing, dimensional, density, surface, flexural or fracture, thermal-cycle, and functional results, plus deviations and final disposition.
If this question concerns a failure mechanism, compare the ceramic 3D printing service after the suspected cause and test condition are identified.
For a controlled production decision, request the vat photopolymerization service when the final state and deviation path need traceable evidence.
.webp)