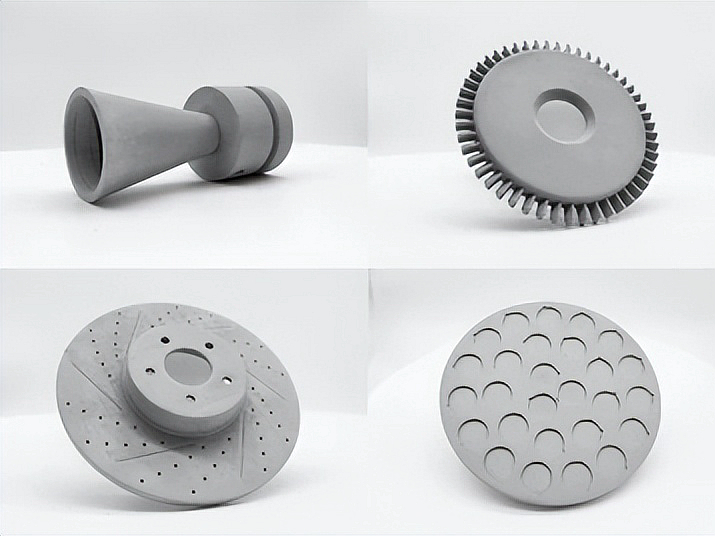
How do ceramics perform in high-temperature and high-stress applications?
How do ceramics perform in high-temperature and high-stress applications?
Ceramics can perform well in high-temperature or high-stress applications when material, atmosphere, thermal gradient, flaw condition, geometry, and loading are defined. Alumina, zirconia, silica, silicon nitride, and silicon carbide do not share one service limit. Ceramic 3D printing also adds a green-body, debinding, sintering or firing, shrinkage, density, and surface history. A fired part may retain heat and chemical advantages while remaining sensitive to tensile flaws or thermal shock. Use a project-specific test and acceptance boundary rather than a generic temperature claim.
Thermal Stability and Material Choice
Alumina can be screened for electrical insulation and chemical stability, silicon carbide for selected high-temperature, wear, or chemical environments, and silicon nitride for applications needing a combination of mechanical and thermal-shock behavior. Zirconia can provide thermal insulation or wear performance depending on its stabilized phase, while silica has its own expansion and firing boundary. The result depends on porosity, additives, surface, atmosphere, temperature, dwell, and thermal cycling. For a furnace fixture, nozzle, or insulator, choose the material only when these variables are specified; verify fired density, surface, dimensions, and thermal response.
Thermal Shock and Thermal Gradients
Rapid heating or cooling creates a temperature gradient between the surface and interior. Because ceramics have limited plastic relaxation, that gradient can generate tensile stress and initiate a flaw. Feedstock packing, wall thickness, pore distribution, edge radius, support, firing profile, and cooling rate influence the result. A printed lattice may reduce thermal mass but can also create thin struts and inspection limits. For a silicon nitride or alumina thermal-cycle component, choose geometry and route together; verify thermal cycles using the final fired and finished surface.
High Stress, Wear, and Fracture
Ceramic strength is flaw-sensitive and often statistically distributed. A pore, debinding crack, surface scratch, edge chip, or machining mark can control fracture even when bulk density appears acceptable. Compression-dominated loading may be suitable where direct tension or impact is not, but the load path and mounting must prevent unintended tensile stress. For a zirconia wear insert or silicon carbide flow component, choose a route when contact load, pressure, surface, temperature, and flaw inspection are defined; verify flexural, fracture, wear, pressure, or life data under the intended condition.
Aerospace, Energy, and Electronics Boundaries
For an aerospace heat shield, nozzle, or insulator, choose alumina, silicon nitride, silicon carbide, or another qualified material only when atmosphere, thermal cycle, stress, porosity, oxidation, and project-specific acceptance criteria are defined; verify the fired final state and thermal or fracture evidence. For an electronics insulator, choose alumina or another ceramic only when dielectric path, contamination, fit, surface, and thermal cycling are specified; verify insulation after firing and finishing. For an energy pressure or flow component, verify density, leakage, flow, thermal cycle, and surface flaw condition.
Verification and RFQ
Use ASTM C1161 or another suitable flexural method, ASTM C373 or another suitable density and apparent-porosity method, and a project-defined thermal-cycle, oxidation, pressure, wear, or fracture method where applicable. The standard does not supply a universal acceptance limit. Record specimen orientation, fired condition, surface, temperature, stress, cycle count, exposure, measurement uncertainty, and failure criterion. A green-body result cannot substitute for the fired state.
Provide ceramic grade, feedstock lot, route, CAD and drawing revision, quantity, green handling, debinding, firing, shrinkage, density, porosity, dimensions, load, temperature, atmosphere, fluid, pressure, surface, inspection access, schedule, and approval authority. Request process and furnace records, final measurements, surface inspection, flexural or fracture data, thermal-cycle or pressure tests, deviations, and final disposition. Release only when the evidence matches the actual service boundary.
Before approving this application route, check the ceramic 3D printing service against the part's operating condition, critical feature, and acceptance limit.
For supplier comparison, use the vat photopolymerization service to separate a process capability statement from evidence on the completed part.
.webp)