What 3D printing technologies are most suitable for stainless steel?
What 3D printing technologies are most suitable for stainless steel?
Powder-bed fusion is usually the first process family to evaluate for complex stainless steel parts because it can form detailed geometry with a consistent layer-by-layer route. DMLS, SLM, and similar commercial terms describe related metal powder-bed approaches, but the actual decision depends on machine, powder, parameter qualification, geometry, and final treatment.
How do the routes differ?
Laser powder-bed processes melt selected regions of a powder layer and repeat the cycle. The name used by a supplier may refer to a specific machine or a commercial process label, so the buyer should ask for the actual machine family, powder specification, layer strategy, and qualified material condition.
DED adds material from a nozzle or feeder and can be attractive for repair, larger sections, or adding features to an existing substrate. It usually has a different resolution, heat input, surface state, and machining allowance from powder-bed work. Directed energy deposition should therefore be compared by finished function, not by the label alone.
What decides the best route?
For a small 17-4PH bracket, laser powder-bed fusion may suit detailed geometry, but its thermal gradient and support strategy still influence distortion and fatigue surfaces. For a larger repair, DED changes the heat-affected zone and machining allowance. Compare the actual feature, build direction, treatment, and final inspection method before selecting the process name.
Feature size, internal channels, wall thickness, part envelope, quantity, support access, surface requirement, and machining allowance drive the route. A small complex manifold may favor powder-bed fusion, while a large repair feature may favor DED. A simple high-volume item may favor machining, forming, or casting.
The design must also allow powder removal and inspection. A channel that is theoretically printable but cannot be cleaned, measured, or leak-tested is not production-ready.
What should the quote specify?
Ask for the process name, machine envelope, material grade and powder lot, orientation, support strategy, post-processing, dimensional capability for critical features, and the inspection records included. State whether the result must be as-built, stress-relieved, heat-treated, or machined.
If the route is selected for mechanical performance, specify specimen orientation and the final state for testing. If it is selected for a channel, specify the pressure, fluid, test method, and accessible cleaning path.
Commercial names such as DMLS and SLM can describe closely related laser powder-bed approaches, but a buyer should not treat the names as a qualification. Ask for the actual machine, laser configuration, powder specification, layer strategy, qualified parameter set, build envelope, and the material condition represented by the data. Two machines using the same nominal 316L designation may produce different surface, density, and mechanical results if their parameters and post-processing differ.
DED is a different decision because material is delivered to a melt pool through a nozzle or feeder. It can suit larger sections and repairs, but it generally has a different resolution, surface condition, heat-affected zone, and machining allowance. A hybrid route may be attractive when only a local feature is complex. The buyer must inspect the transition between deposited and parent material and define how the final datum is created.
Process selection should begin with a map of the geometry. Mark thin walls, overhangs, enclosed volumes, powder escape routes, support contacts, machined faces, and inspection blind spots. Then map quantity, envelope, and the required final surface. This often narrows the route more effectively than asking which technology has the highest nominal resolution. A simple block with tight bores may still belong to CNC machining.
Qualification should use a representative build strategy. Record orientation, material lot, treatment, specimen direction, and the relation between a witness specimen and the part. For hidden geometry, add CT, radiography, or a functional test only when it addresses a real risk. A process page can explain the family; it cannot replace the project acceptance plan.
A route review should include the machine envelope, powder or wire availability, support removal, treatment, machining, and inspection access. Ask for a fallback route if the part cannot be built in the first orientation.
The final quotation should name what is guaranteed and what remains a development assumption. This is particularly important when the title of a process suggests more precision or density than the project has demonstrated.
Technology selection should be expressed as a sequence: choose the geometry route, qualify material and parameters, choose orientation and supports, complete treatment and machining, then test the final state. A process name without this sequence leaves the buyer unable to judge the quote.
DMLS, SLM, and related labels are not a substitute for machine-specific qualification. Compare laser or energy source, powder specification, layer strategy, orientation, support removal, and treatment. DED may be better for a large repair, but its deposited zone, heat-affected zone, and machining allowance need a different inspection plan.
The route should be selected after mapping the critical features. Mark the surfaces that need machining, the cavities that need cleaning, the regions that need NDT, and the features that carry the load. Then request a representative first article rather than relying on a generic process brochure.
Process choice and build evidence
Process selection should follow the feature that controls acceptance. Laser powder-bed fusion is usually evaluated for fine stainless geometry because its layer and scan strategy can form small features, but the result is sensitive to orientation, supports, thermal gradients, and powder-removal access. DED may be better for a larger repair or added feature, yet the deposited interface and heat-affected zone become part of the inspection plan. metal powder-bed fusion
Ask the supplier to identify the machine family, powder or wire lot, qualified parameter set, orientation, support plan, and final state. For a hidden channel, the route is incomplete until cleaning and leak testing are defined. For a precipitation-hardening grade, surface treatment must state whether the quoted dimensions and properties are before or after treatment. A route is accepted only when the chosen inspection can reach the feature that drove the decision.
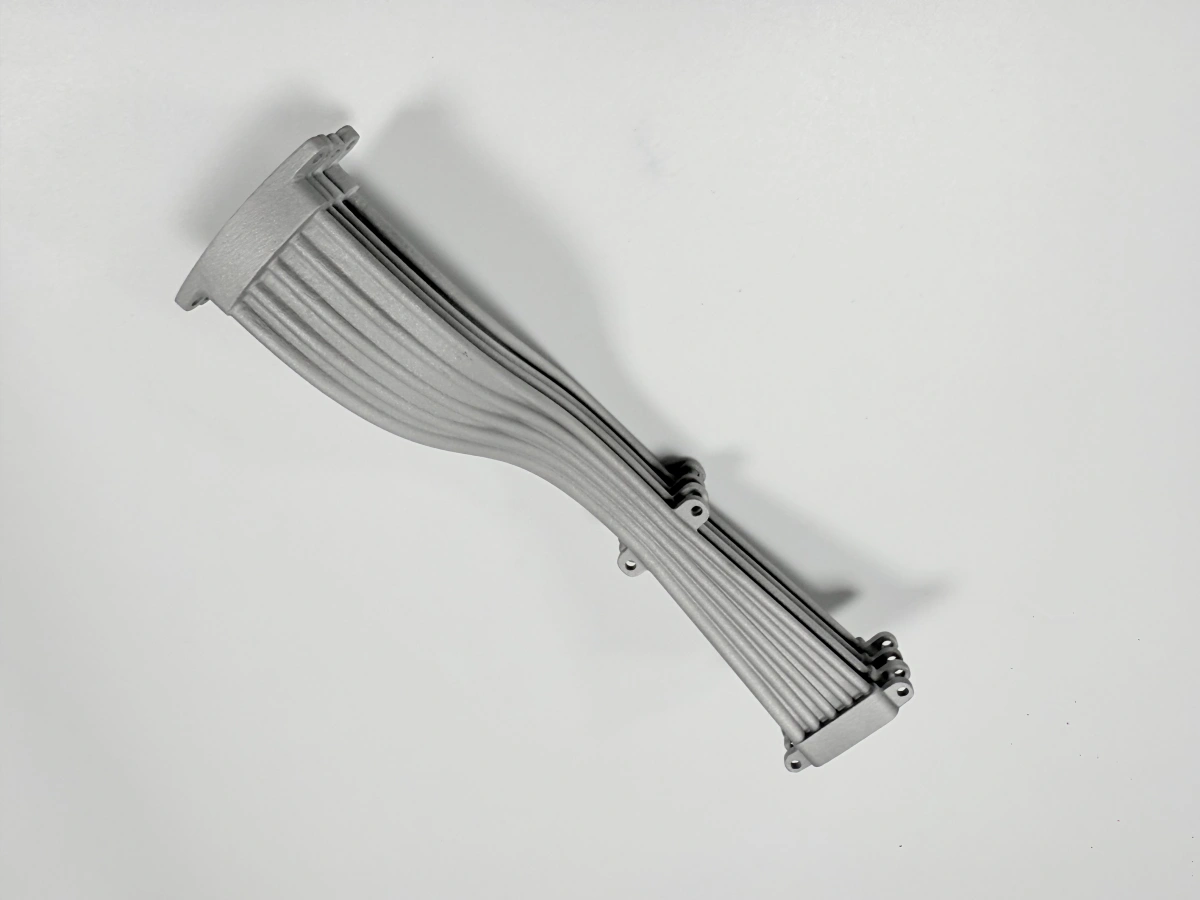
.webp)