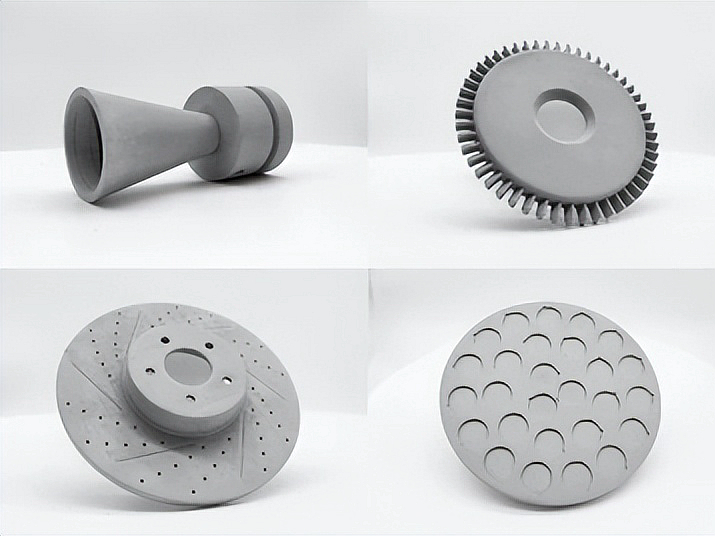
What are the main advantages of ceramic 3D printing compared to traditional methods?
What are the main advantages of ceramic 3D printing compared to traditional methods?
The short answer is yes: ceramic 3D printing can be advantageous when a custom part needs complex geometry, a low production quantity, a controlled ceramic material, or a design iteration that would be expensive to tool by pressing, casting, or machining. Alumina, zirconia, silica, silicon nitride, and silicon carbide have different thermal, electrical, wear, and fracture behavior. The advantage is conditional because the printed shape must pass through a green body, debinding, sintering or firing, and final inspection. Compare the complete fired route, not only the forming step.
Geometry and Design Freedom
Ceramic SLA or DLP can cure a particle-filled slurry into fine green-body features, while binder jetting and material extrusion create geometry through powder binding or bead deposition. These mechanisms can produce channels, lattices, thin walls, hollow forms, and consolidated structures that may be difficult to press or machine. The same features can trap binder, distort during firing, or hide a flaw. A complex channel is useful only when the fired passage remains open, cleanable, measurable, and functionally tested.
For an aerospace insulator or thermal-management form, choose ceramic printing when internal geometry has a defined thermal or electrical function and the project can control green-body support, debinding, firing, porosity, and thermal cycling; verify the fired part. For an art or design object, select SLA/DLP, binder jetting, or material extrusion when the visual form and batch size justify the route; verify fired dimensions, surface, glaze, and appearance after cooling. Geometry is an advantage only when the final state retains the intended function.
Low Tooling Commitment and Customization
Traditional ceramic pressing or casting may require molds, dies, cores, or dedicated fixtures. Additive manufacturing can use a digital geometry for a one-off model, custom pattern, patient-specific form, or small series without creating a new hard tool for every revision. The time benefit still includes feedstock preparation, support, drying, debinding, furnace capacity, firing, finishing, and inspection. A fast green-body build is not automatically a fast accepted ceramic part.
For a custom electrical housing, choose vat photopolymerization when fine detail and fit matter and the slurry, cure, debinding, and fired density are qualified; verify dielectric or insulation performance after firing. For a wear insert, choose a zirconia, alumina, silicon nitride, or silicon carbide route only when edge quality, density, thermal cycle, and wear method are specified. The tooling saving must be compared with furnace and quality costs at the actual quantity.
Material Performance and Material Efficiency
Ceramics can provide electrical insulation, chemical stability, high hardness, wear resistance, low or tailored thermal expansion, or high-temperature capability. Alumina and zirconia are not interchangeable, and silicon nitride and silicon carbide have different oxidation, fracture, and thermal-shock boundaries. Additive manufacturing can reduce billet or mold waste in a near-net geometry, but slurry loss, powder handling, support, failed firing, machining, and scrap must be counted. A bulk material property does not establish a printed part's result.
A digital record can connect material lot, solids loading, print parameters, green-body condition, debinding profile, furnace load, firing atmosphere, shrinkage, finishing, and inspection. That traceability supports repeatability, but it does not prove density, dielectric performance, thermal shock, or fracture resistance. Request evidence for the final fired and finished state.
Shrinkage, Brittleness, and Post-Processing
Debinding and sintering can cause substantial dimensional change, and nonuniform packing or section thickness can produce warpage or cracks. A ceramic may carry high compression but remain sensitive to a tensile surface flaw, edge chip, pore, or sharp corner. Grinding, polishing, glazing, or surface treatment can improve a functional surface while changing dimensions or introducing damage. Inspect after the final operation that affects the critical feature.
For an RFQ, provide ceramic grade, feedstock and lot, process route, CAD and drawing revision, quantity, green-body handling, shrinkage allowance, fired dimensions, density or porosity, load, temperature, atmosphere, fluid, pressure, electrical requirement, surface, cleaning or sterilization, inspection access, schedule, and approval authority. Request process, debinding, firing, dimensional, density, surface, flexural or fracture, thermal-cycle, and functional records. Ceramic 3D printing is the better route only when the accepted fired part meets the project boundary.
For a primary route decision, use the ceramic 3D printing service after the material, geometry, and service condition for this question are defined.
For downstream verification, consult the vat photopolymerization service when the final process state and acceptance evidence for this question must be recorded.
.webp)