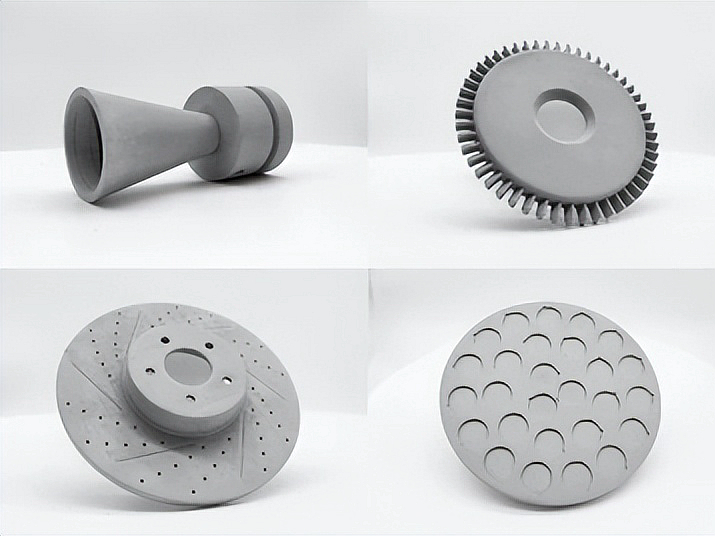
How does ceramic 3D printing benefit industries like aerospace and medical?
How does ceramic 3D printing benefit industries like aerospace and medical?
The short answer is that ceramic 3D printing can benefit aerospace, medical, electronics, energy, tooling, and art users when a controlled ceramic material and custom geometry solve a defined problem. Alumina, zirconia, silica, silicon nitride, and silicon carbide offer different combinations of insulation, wear, thermal-shock, chemical, or fracture behavior. Applications cannot be approved from a material name alone because SLA, DLP, binder jetting, and extrusion create a green body that must be debound and sintered or fired. The final application boundary includes fired density, porosity, dimensions, surface, and test condition.
Aerospace and Energy
Aerospace and energy programs may screen alumina for insulation, silicon nitride for selected thermal-shock or mechanical functions, silicon carbide for high-temperature or wear environments, and zirconia for thermal or wear roles. The mechanism is application-specific: particle packing and furnace profile determine porosity and shrinkage, while surface flaws and thermal gradients influence fracture and thermal-cycle life. For an aerospace insulator, nozzle, heat shield, or energy fixture, choose ceramic printing only when temperature, atmosphere, stress, thermal shock, oxidation, porosity, inspection access, and project-specific qualification are defined; verify the fired final state. Industry use is not approval evidence.
Medical and Dental Development
Medical and dental development may use zirconia, alumina, hydroxyapatite, or other ceramics for patient-specific models, dental forms, selected guides, porous research structures, or implant development. A printed green body is not a medical device, and a fired ceramic's biocompatibility cannot be inferred from the process. Surface, residual binder, cleaning, sterilization, chemistry, density, porosity, fracture behavior, traceability, and regulatory documentation must be addressed. For a medical or dental part, choose a route only after project-specific qualification defines material classification, cleaning, sterilization, surface, dimensional, biological, and acceptance requirements; verify the final state. A generic medical example is not approval evidence.
Electronics and Thermal Management
Electronics users may screen alumina or another ceramic for insulators, sensor housings, dielectric structures, and thermal isolation when geometry or customization matters. Ceramic-filled SLA/DLP can provide detail, but cure, debinding, firing, and porosity affect dielectric path and fit. For an electrical insulator, choose the route when dielectric requirement, creepage, contamination, fired density, thermal cycling, and assembly tolerance are specified; verify insulation and final dimensions after finishing. Thermal-management use also needs conductivity, interface, temperature cycle, and surface evidence.
Tooling, Wear, and Art
Tooling users may select alumina, zirconia, silicon nitride, or silicon carbide for custom inserts, wear surfaces, patterns, or high-temperature fixtures when hardness or chemical resistance justifies the brittleness risk. Art and design users may prioritize hollow form, texture, color, or one-off production; material extrusion, binder jetting, and SLA/DLP have different green handling and fired-shrinkage behavior. For a wear insert, choose a route when contact load, edge condition, thermal cycle, and life test are known; for an art object, verify fired shape, glaze or finish, and visual acceptance after cooling.
Industry Selection and RFQ
Compare ceramic SLA, DLP, binder jetting, material extrusion, and any specialized route by feedstock, green-body strength, detail, quantity, support, debinding, firing, shrinkage, density, porosity, surface, inspection, and final function. Ceramic 3D printing is a complete conversion chain rather than a forming-only service.
Provide CAD and drawing revision, ceramic grade, feedstock lot, quantity, route, solids loading or powder condition, shrinkage allowance, fired dimensions, density, porosity, load, temperature, atmosphere, fluid, pressure, electrical requirement, surface, cleaning or sterilization, inspection access, schedule, and approval authority. Request process, debinding, firing, dimensional, density, surface, thermal, flexural or fracture, and functional records. Release the industry application only for the final condition supported by those records.
When comparing material capability, use the ceramic 3D printing service after the required property and section condition for this answer are fixed.
When planning the next process step, review the vat photopolymerization service against the final geometry, inspection access, and release evidence described here.
.webp)