What Are The Typical 3D Printing Technologies Used In Custom Parts Manufacturing?
 What Are The Typical 3D Printing Technologies Used In Custom Parts Manufacturing?
The typical 3D printing technology for a custom part depends on material, feature size, build envelope, quantity, orientation, surface requirement, tolerance, post-processing, inspection access, and service load. Powder bed fusion, material extrusion, vat photopolymerization, directed energy deposition, and binder jetting each create a different starting state. A suitable route is not simply the one with the smallest layer or fastest build. It is the route that can produce the required final geometry and material condition with a documented verification path.
A documented route can reduce avoidable rework when the buyer defines the final state before the build and verifies critical features after post-processing. It can preserve a useful internal passage only when the process, cleaning method, inspection access, and acceptance test are selected together. It can shorten iteration for low-volume work when machine capacity, material qualification, and downstream operations are included in the schedule.
Custom manufacturing decisions should begin with the part's failure mode and delivery state. A metal bracket may need fatigue data, heat treatment, machining, and CT or NDT. A polymer fixture may need chemical compatibility, dimensional stability, and low-volume repeatability. A ceramic component may need debinding, firing, shrinkage control, and thermal-shock evidence. Define the final acceptance criteria before comparing process names.
Factors That Control Route Selection
Material determines the available process family and the relevant post-process state. Laser or electron-beam powder bed routes can produce dense metal features, but the final properties depend on powder lot, energy input, orientation, thermal history, and heat treatment. Material extrusion deposits a filament or pellet bead whose layer bonding and cooling history govern anisotropy. Vat photopolymerization forms a cured resin body whose wash and cure condition controls the final response. Binder jetting and ceramic routes add debinding and sintering or firing, so shrinkage becomes a primary design variable.
Geometry changes the practical value of a process. Fine channels, lattices, thin walls, undercuts, and internal cavities may favor a powder bed or vat route, but trapped powder, support access, uncured resin, and inspection limits remain. Large repairs or near-net deposition may favor directed energy deposition, while a large batch of smaller parts may favor binder jetting when shrinkage and density are controlled. Build orientation affects layer direction, support burden, surface quality, and load path; it should be decided with the post-process and inspection plan rather than after the build is complete.
Technology Selection Matrix
Technology | Typical fit | Trade-off to evaluate | Verification focus |
|---|---|---|---|
LPBF or metal PBF | Small to medium metal parts with fine features, internal channels, or low to moderate quantity | Support access, residual stress, roughness, powder removal, and heat-treatment state | Density or defect evidence, material tests, CMM, surface inspection, and functional test |
DED | Large features, repairs, graded deposition, or parts where material is added to a substrate | Bead geometry, dilution, heat input, anisotropy, machining allowance, and distortion | Build record, bonding or NDT evidence, heat history, machining report, and dimensions |
Material extrusion | Polymer fixtures, prototypes, patterns, and low-load custom parts | Layer direction, moisture, warpage, support removal, and surface finish | Condition record, dimensions, flexural or load test, and chemical exposure where relevant |
Vat photopolymerization | Fine-detail models, patterns, housings, and visual or fit prototypes | Residual resin, cure gradient, brittleness, cleaning, and dimensional change | Wash and cure record, hardness or flexural result, fit, and final inspection |
Binder jetting | Batch production of suitable metal or ceramic geometries | Green-body handling, debinding, shrinkage, density variation, and warpage | Furnace record, density, dimensions, porosity, strength, and functional test |
Use the matrix as a screening tool, not as a substitute for process qualification. A route that appears suitable at part level can fail because the smallest channel cannot be cleaned, the final surface cannot be measured, or the post-process changes a seal. Record the selected technology, rejected alternatives, selection reason, and unresolved risk in the project file.
Powder Bed Fusion for Custom Metal Parts
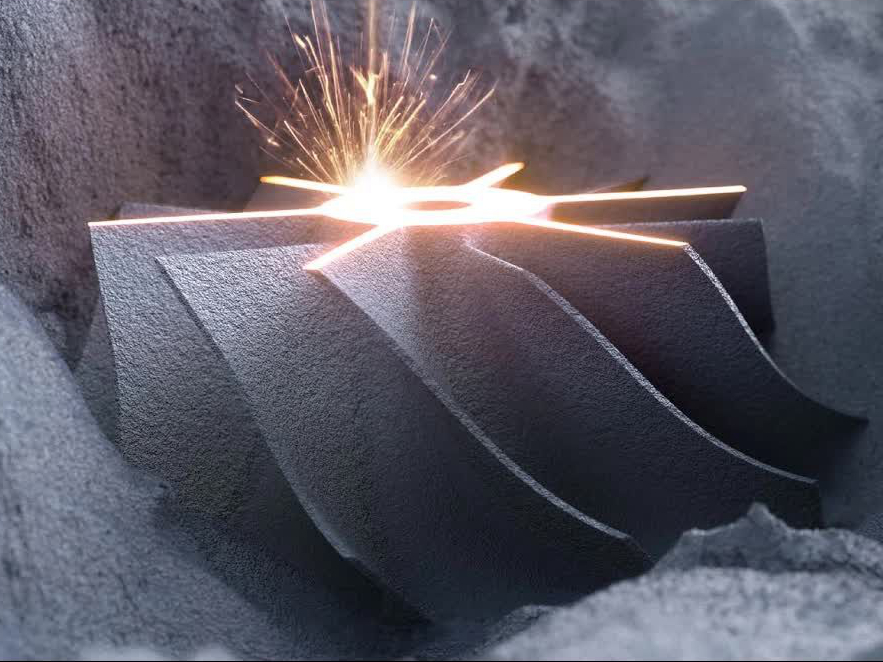
Powder bed fusion includes laser and electron-beam variants. Laser powder bed fusion generally supports fine features and controlled detail, while electron-beam routes may offer a different thermal environment and support strategy. Do not treat LPBF, SLM, and DMLS as identical material specifications. The buyer should identify machine, powder grade and lot, layer thickness, energy or scan strategy, orientation, support design, build plate, and post-build handling.
Metal PBF can create residual stress and rough surfaces. Depowdering and support removal must be completed before a channel or cavity is sealed. Stress relief or a material-specific heat-treatment cycle can change strength, hardness, phase condition, and dimensions. Machining establishes datums and sealing faces, but the allowance must account for distortion and the final sequence. Inspect the material state after all operations that can move or add material.
Polymer Printing for Custom Fixtures and Housings
Material extrusion is useful when the buyer accepts visible layer direction, anisotropic strength, and a defined surface finish. Choose it for fixtures, patterns, covers, or low-load custom parts when the material's temperature, moisture, chemical, and stiffness limits are suitable. Orientation and bead path should follow the load and the support-removal plan. Annealing or drying may change dimensions, so measure after conditioning.
Vat photopolymerization can supply fine detail and a smooth initial surface, but uncured resin, wash chemistry, UV exposure, and thermal post-cure shape the final part. A delicate feature may become brittle after additional cure. Verify the condition at the time of use. Powder-based polymer routes can provide more isotropic behavior in some applications, but depowdering and surface finishing remain part of the design review.
DED, Binder Jetting, and Ceramic Routes
DED is selected when material must be added to a substrate, a large feature is needed, or a repair is more practical than a complete rebuild. The deposited zone may have a different microstructure, dilution, heat history, and machining allowance from the substrate. Control substrate preparation, bead overlap, energy input, interpass temperature, and final heat treatment. Use NDT or microscopy where the bonding and defect risk require it.
Binder jetting and ceramic printing require careful green-body handling, controlled debinding, and sintering or firing. Shrinkage depends on powder loading, packing, furnace profile, support, section thickness, and geometry. A fired ceramic can be dense and strong in compression yet sensitive to a tensile surface flaw. Inspect density, porosity, dimensions, and thermal or pressure function in the final state.
Post-Processing and Inspection Are Part of Technology Choice
A technology comparison is incomplete until it includes the downstream route. CNC machining may be essential for a datum or seal, but it requires stock and tool access. Surface finishing can change roughness, edge radius, flow area, or coating adhesion. Heat treatment, cure, HIP, debinding, sintering, and firing can change dimensions or mechanical response. Use a process traveler that records each state and the inspection performed before the next operation hides a defect.
Use ISO/ASTM 52900 for additive-manufacturing terminology when useful, but do not treat it as a part acceptance standard. Apply the relevant material or product standard and the buyer drawing. Inspection may include CMM, roughness measurement, CT, radiography, microscopy, NDT, hardness, tensile, flexural, leak, pressure, flow, or thermal testing. The method must resolve the risk at the actual feature. A coupon can support process development without qualifying every custom geometry.
Application Decision and RFQ
For an aerospace bracket or duct, select metal PBF when fine features and internal geometry justify the route and the project can control orientation, heat treatment, machining, fatigue, and inspection. Verify the final material state, datums, surface, and load-related evidence before release. For an automotive housing or fluid manifold, select PBF, DED, or another route only when passage cleanliness, flow, leakage, and fit are part of the planned final state. Verify the finished internal feature after cleaning, finishing, and machining. For a medical or energy component, choose a route only when material compatibility, sterilization or fluid chemistry, temperature, pressure, traceability, and quantity are defined; verify the applicable functional and documentation requirements against the project specification.
For an RFQ, provide CAD and drawing revision, material grade, feedstock lot, required quantity, build envelope, critical features, orientation limits, supports, tolerances, surface requirements, load, temperature, pressure, fluid, cleaning or sterilization, post-process sequence, inspection access, schedule, and approval authority. Request process parameters, build and feedstock records, heat or cure history, support or depowdering evidence, machining report, surface map, material tests, NDT or CT, dimensional results, functional tests, deviations, and final disposition. Release the route only when the complete manufactured state meets the stated criteria.
FAQs
What Are the Key Benefits of Using 3D Printing for Custom Parts Manufacturing?
Which Industries Benefit Most from 3D Printing Technologies?
What Are the Most Common 3D Printing Technologies for Custom Parts Manufacturing?
What Are the Challenges of 3D Printing in Custom Parts Manufacturing, and How Can They Be Addressed?
How Does the Cost of 3D Printing Compare to Traditional Manufacturing for Low-Volume Production?
For the primary route, review the material extrusion service when this requirement is part of the release plan.
For the downstream condition, compare the powder-bed fusion service before fixing the final acceptance state.
For the finishing and inspection boundary, use the vat photopolymerization service when the geometry requires it.
Additive route selection can reduce tooling commitment only when the part quantity, geometry, material, and finishing route are defined; verify lead time and final cost from a comparable RFQ. It can improve iteration speed for a qualified low-volume design, but it cannot make every material or tolerance economical; inspect the final state and compare the full process chain. It can support production repeatability only when the machine, feedstock, build orientation, post-processing, and acceptance record are controlled.
For a low-volume aerospace bracket, choose a powder-bed route when topology and buy-to-fly reduction justify support removal and inspection; verify dimensions, density, and the final material condition. For a production fixture, choose material extrusion when size, cost, and load direction fit the process; verify stiffness, thermal exposure, and repeatability. For a conformal-cooling insert, choose a metal route only when channel access, leakage testing, heat treatment, machining allowance, and the mold acceptance plan are defined.