What industries benefit from combining 3D printing and EDM?
What industries benefit from combining 3D printing and EDM?
Industries benefit from combining 3D printing and EDM when additive manufacturing provides a complex near-net form and EDM provides controlled access to a conductive hard-to-machine detail. Aerospace, medical development, automotive tooling, energy, and industrial equipment can use the combination for thin contours, narrow slots, blind cavities, inserts, cooling features, and hard alloy surfaces. The benefit is application-specific: additive manufacturing does not make every internal feature accessible, and EDM does not remove the need for cleaning, surface-integrity control, or final inspection. A buyer should choose the hybrid route after reviewing access, material state, service function, quantity, and evidence.
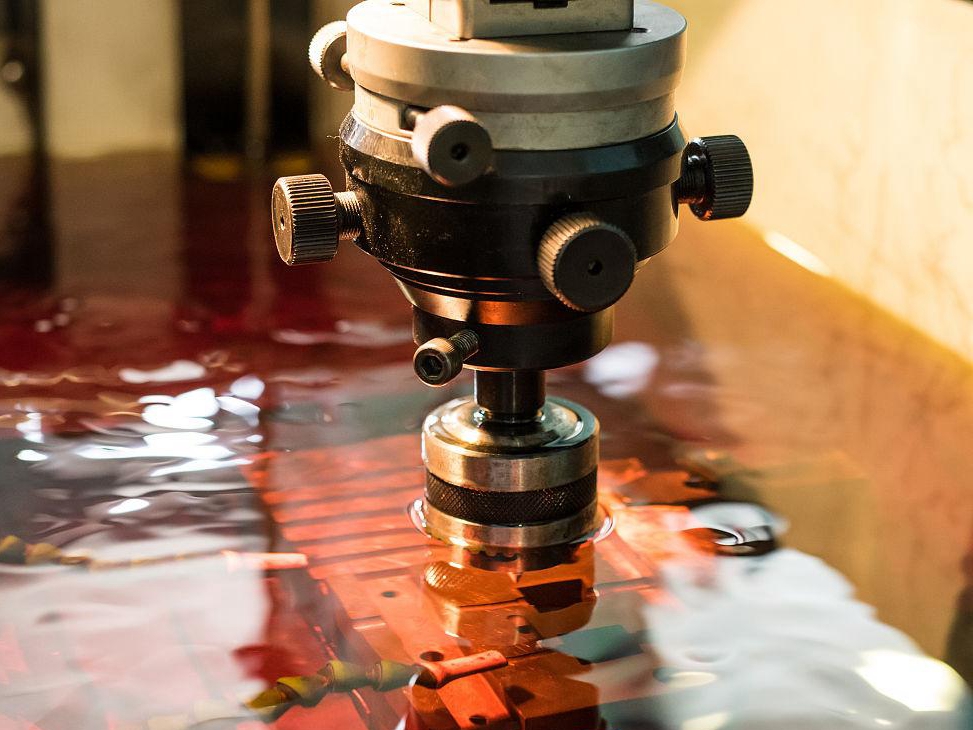
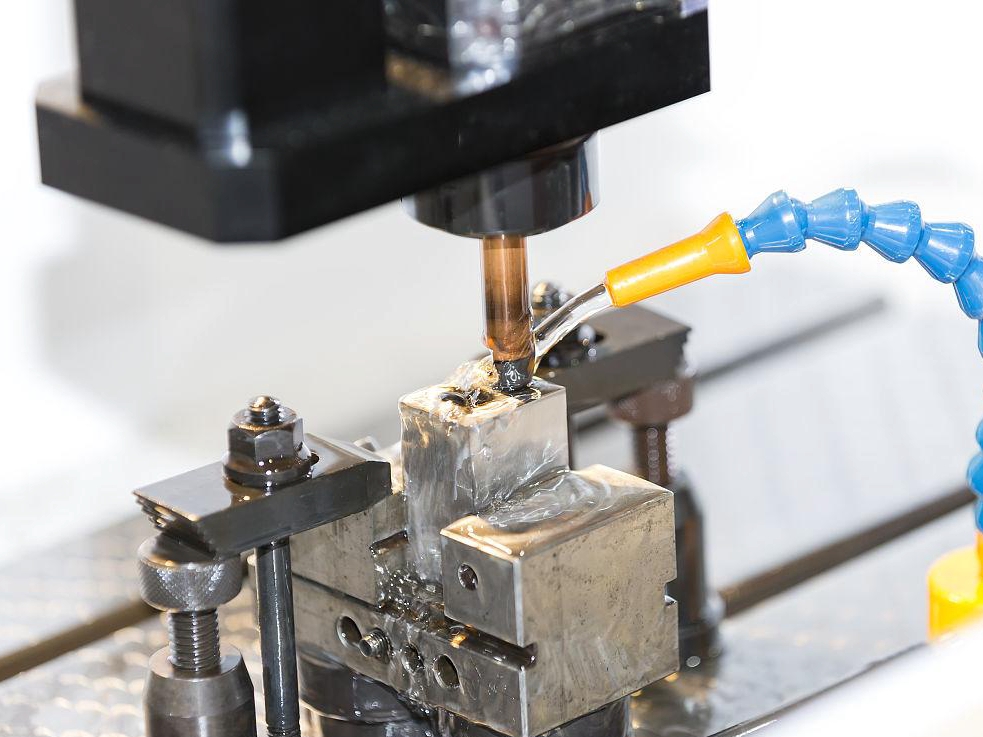
The hybrid mechanism is sequential. Additive manufacturing places material where the final form needs it, while EDM removes a controlled allowance from a conductive detail. The discharge gap creates localized thermal events, and dielectric flushing controls debris; the printed layer structure and residual stress determine how the part responds. A later EDM finishing operation can add value only when the access, cleaning, and inspection path is preserved through the sequence.
Process Window and Qualification
A hybrid route is qualified through linked records. The additive build establishes layer direction, density, residual stress, and support history; EDM then controls the discharge gap, pulse energy, electrode or wire access, and flushing. A later treatment can change stock or surface chemistry. For an aerospace component, qualify the complete sequence on representative material and geometry, then inspect the final condition. For an industrial fluid component, correlate the dimensional and surface results with the actual flow or leak test. A process name alone cannot establish application fitness.
The discharge mechanism also determines what each industry must verify. A stable gap can reduce force-related damage only when the feature is conductive and accessible, while poor flushing can create pits or residue. An additive layer boundary or pore can remain a fatigue risk after the contour looks accurate. Record the build state, EDM state, cleaning state, and final state separately before comparing the result with the service requirement.
Aerospace and Energy
Aerospace fuel injectors, manifolds, cooling inserts, turbine details, and actuator components may combine nickel or titanium alloys with thin walls and fatigue-sensitive features. Print the manifold or lattice near net shape, then choose wire EDM for an accessible slot or contour when cutter force or tool wear threatens the geometry. Choose sinker EDM for a blind detail only when the electrode can reach it and debris can be flushed. Verify profile, recast or HAZ, cleanliness, flow, leakage, and fatigue-relevant condition according to the project.
Energy equipment can have hard conductive inserts, fluid passages, and high-temperature service. Define pressure, temperature, fluid, dwell, cleaning, and acceptance authority. A bright entrance or coupon cannot prove the bottom of a passage. If a heat-treatment operation changes dimensions or residual stress after EDM, repeat inspection in the final state.
Medical Development
Medical-development instruments, fluid-handling prototypes, and development implant features may benefit from additive design freedom plus EDM edge or cavity control. EDM can reach a conductive hard alloy without continuous cutter contact, but its surface may include recast, residue, microcracks, or altered chemistry. Define contact surface, alloy grade, printed and thermal states, cleaning chemistry, sterilization exposure, roughness, edge condition, residue testing, and development approval. A precise surface is not evidence of biocompatibility or clinical acceptance.
Tooling and Automotive
Automotive mold inserts, die components, punches, and conformal-cooling tooling can combine an additively built form with sinker EDM on a hardened cavity. The electrode form, wear compensation, flushing, corner strategy, polishing allowance, and coating thickness determine the final tool. Use surface treatment only within a defined allowance and measure after the complete sequence. For open datums or stable faces, CNC machining may be simpler; assign each critical feature to the route that can be measured and accepted.
Hybrid RFQ and Verification
Provide CAD and drawing revision, material grade and lot, build orientation, heat-treatment condition, feature access, minimum wall thickness, allowance, quantity, EDM mode, wire or electrode plan, surface condition, recast or HAZ limit, cleaning, functional load or fluid, inspection method, and acceptance authority. Ask for the additive build record, EDM parameter family, workholding datum, dimensional report, surface-integrity evidence, cleaning record, and nonconformance disposition.
For an aerospace cooling insert, choose wire EDM when the profile is accessible and low cutter force protects the wall; verify profile, recast, cleanliness, and flow. For a tooling cavity, choose sinker EDM when the electrode reaches the blind feature; verify corners, roughness, and final dimensions. For a medical-development component, select EDM only after contact and cleaning boundaries are defined. The industries that benefit most are those that treat additive design and EDM finishing as one verifiable manufacturing chain. Keep the additive build record, EDM parameter record, cleaning record, and final inspection report linked to the same part or lot so a later review can trace each decision.
For RFQ preparation, request the electrical discharge machining edm after the buyer defines the material state, quantity, and required verification method.
For final release, compare the CNC machining service with the inspection record, service condition, and disposition of any unresolved risk.