How does Electron Beam Melting (EBM) benefit carbon steel parts for aerospace applications?
How does Electron Beam Melting (EBM) benefit carbon steel parts for aerospace applications?
EBM can benefit a carbon steel aerospace part when a supplier has a qualified EBM material route for the exact grade and the design can accept the process surface, build envelope, powder-removal needs, and final machining. Its vacuum environment and elevated build temperature can reduce some thermal-gradient and oxidation concerns, but they do not prove low residual stress, fatigue life, or aerospace acceptance by themselves. The benefit must therefore be demonstrated through alloy-specific records, representative geometry, post-processing, and an approved verification plan.
What the EBM Thermal Environment Changes
EBM uses an electron beam to melt metal powder in a vacuum while the powder bed is maintained at an elevated temperature. Compared with a colder laser powder bed process, this thermal history can reduce the difference between a newly melted track and the surrounding material. That may reduce certain distortion or residual-stress risks for a qualified material and geometry. It does not eliminate thermal strain, phase changes, surface roughness, or dimensional change during heat treatment.
Vacuum processing also limits exposure to air during melting. This can be helpful for oxidation-sensitive feedstock, but the powder specification, vacuum record, beam calibration, and contamination controls still matter. A buyer should ask which carbon steel grade is qualified on which machine and whether the result is as-built, stress relieved, quenched and tempered, or otherwise treated. The carbon steel additive-manufacturing service should be evaluated as a complete process route, not as an EBM label.
Because EBM manages the powder-bed thermal gradient in a vacuum, the carbon steel thermal history can differ from a laser build in residual stress, surface condition, and phase response. That mechanism may be useful only when the exact grade, machine, orientation, and post-processing route have supporting evidence.
Where EBM May Fit in an Aerospace Program
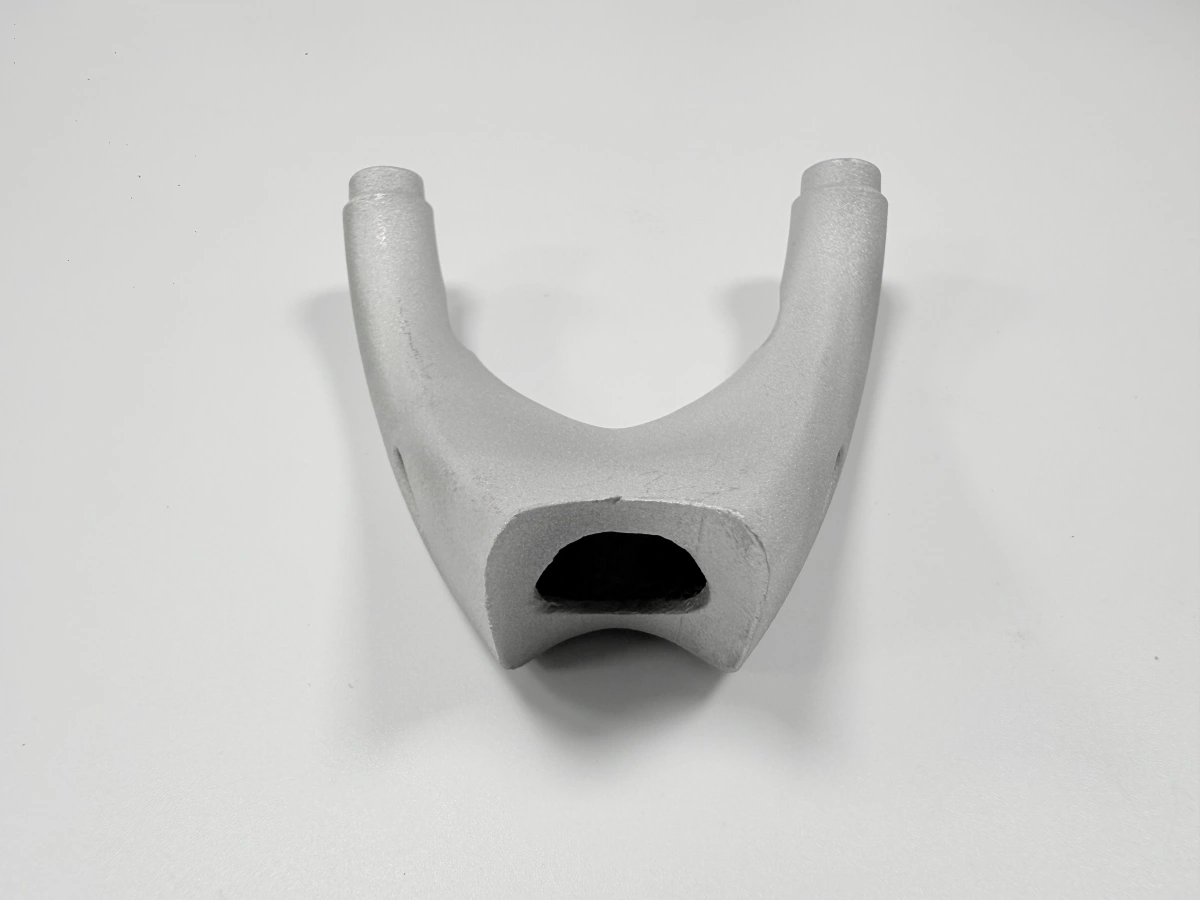
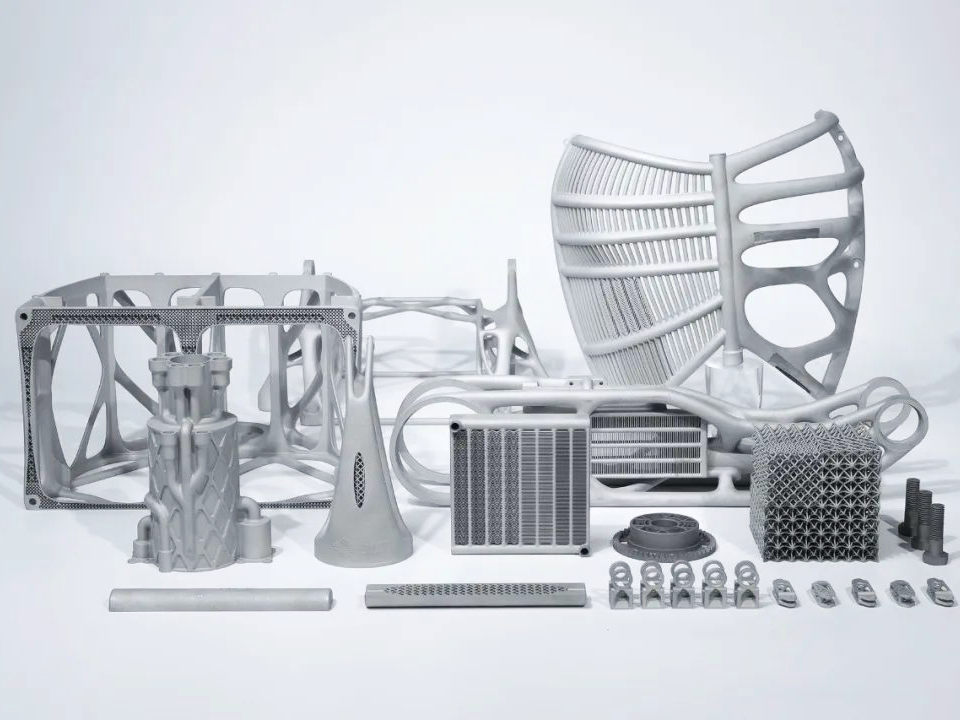
EBM may be screened for a large structural bracket, a mounting interface, or a thermally cycled support when the part benefits from additive geometry and the qualified material data covers the required load path. A topology-optimized shape can reduce mass or consolidate interfaces, but the design must leave access for powder removal, support strategy, machining, and inspection. EBM is not automatically appropriate for a thin, highly polished sealing surface or a small feature whose tolerance is tighter than the process and finishing route can control.
For a high-cycle bracket, the key question is not whether the process can produce a dense-looking sample. It is whether the actual orientation, surface condition, stress concentration, heat treatment, and machining sequence are represented in the fatigue evidence. For a thermally cycled component, include the service temperature range, dwell time, vibration, and any oxidation or fluid exposure in the validation plan. A coupon from a different section thickness can support process monitoring but cannot release a geometry with a different notch or surface condition.
Carbon Steel Grade and Aerospace Limits
AISI 4130, AISI 4140, H13, D2, or 20MnCr5 may be discussed for different functions, but they are not interchangeable aerospace materials. AISI 4130 may suit a toughness or joining requirement; AISI 4140 may be screened for a heat-treated strength and toughness balance; H13 is a hot-work tool steel and D2 is a wear-focused tool steel; 20MnCr5 requires a case-hardening route when the surface and core need different properties. The design authority must confirm whether the grade and final condition are allowed for the component.
Heat treatment can improve the required material condition only when the cycle is matched to the grade and the printed microstructure. It can also cause distortion or expose cracks. Specify furnace atmosphere, heating and cooling controls, quench or tempering requirements, hardness or tensile criteria, and dimensional inspection after treatment. If a heat-treatment service is included, request the actual cycle record and lot traceability. “Aerospace grade” should not be used as a substitute for a material specification or approval record.
Failure Modes and Controls for EBM Parts
Potential failure modes include lack of fusion, keyhole or gas porosity, surface-connected defects, powder trapped in internal passages, distortion, and cracking during thermal processing. Control starts with a qualified powder size and chemistry, vacuum and beam records, parameter control, and build-orientation rules. Then inspect the final geometry with a method capable of finding the relevant risk. CT may help with selected internal features, while metallography or sectioning may be needed for process qualification. Neither method should be selected without considering resolution and the location of the defect.
Surface roughness can act as a fatigue notch, especially on an as-built tensile or bracket surface. Allow machining, blasting, or another controlled finish only where the geometry and wall thickness support it, and repeat dimensional inspection after finishing. A CNC machining step can establish a datum or remove an allowance; it cannot repair internal lack of fusion or prove a bond. If inspection finds a nonconformance, hold the part and obtain an engineering disposition instead of changing the acceptance criterion.
Verification Evidence and RFQ Inputs
For tensile evidence, ASTM E8/E8M may be considered when the material specification accepts that method. ASTM F3122 can provide a reference framework for evaluating metal additive-manufacturing materials, but the aerospace program must define the applicable specification, specimen orientation, thermal state, test temperature, and acceptance limits. Fatigue, fracture, hardness, metallography, dimensional, and functional tests should be selected from the actual failure risk. Record the machine, powder lot, vacuum history, build orientation, support removal, and post-processing.
An aerospace RFQ should include the CAD and drawing revision, alloy, quantity, load spectrum, temperature and atmosphere, critical datums, minimum wall, internal channels, surface requirement, machining allowance, inspection method, documentation, qualification authority, and delivery milestone. Ask for a route comparison if EBM and laser powder bed fusion are both being considered. Release should depend on the agreed dimensional and material evidence, not on the general claim that EBM reduces residual stress. That is how a potential process benefit becomes a defensible aerospace manufacturing decision.
If this question concerns a failure mechanism, compare the carbon steel 3d printing after the suspected cause and test condition are identified.
For a controlled production decision, request the powder-bed fusion service when the final state and deviation path need traceable evidence.