Stainless steel 3D printing compared to traditional methods in terms of strength and performance?
Stainless Steel 3D Printing Compared to Traditional Methods in Terms of Strength and Performance
Comparable performance requires qualification
3D printed stainless steel can meet a required mechanical target when the alloy, machine parameters, orientation, thermal treatment, surface condition, and inspection plan are qualified together. SUS316L or SUS17-4PH behave differently; when using Powder Bed Fusion, compare coupon orientation and final geometry. Do not transfer a coupon result to a complex part without representative evidence; heat treatment and HIP are not a substitute for testing the finished part.
Enhanced Performance Through Design Freedom
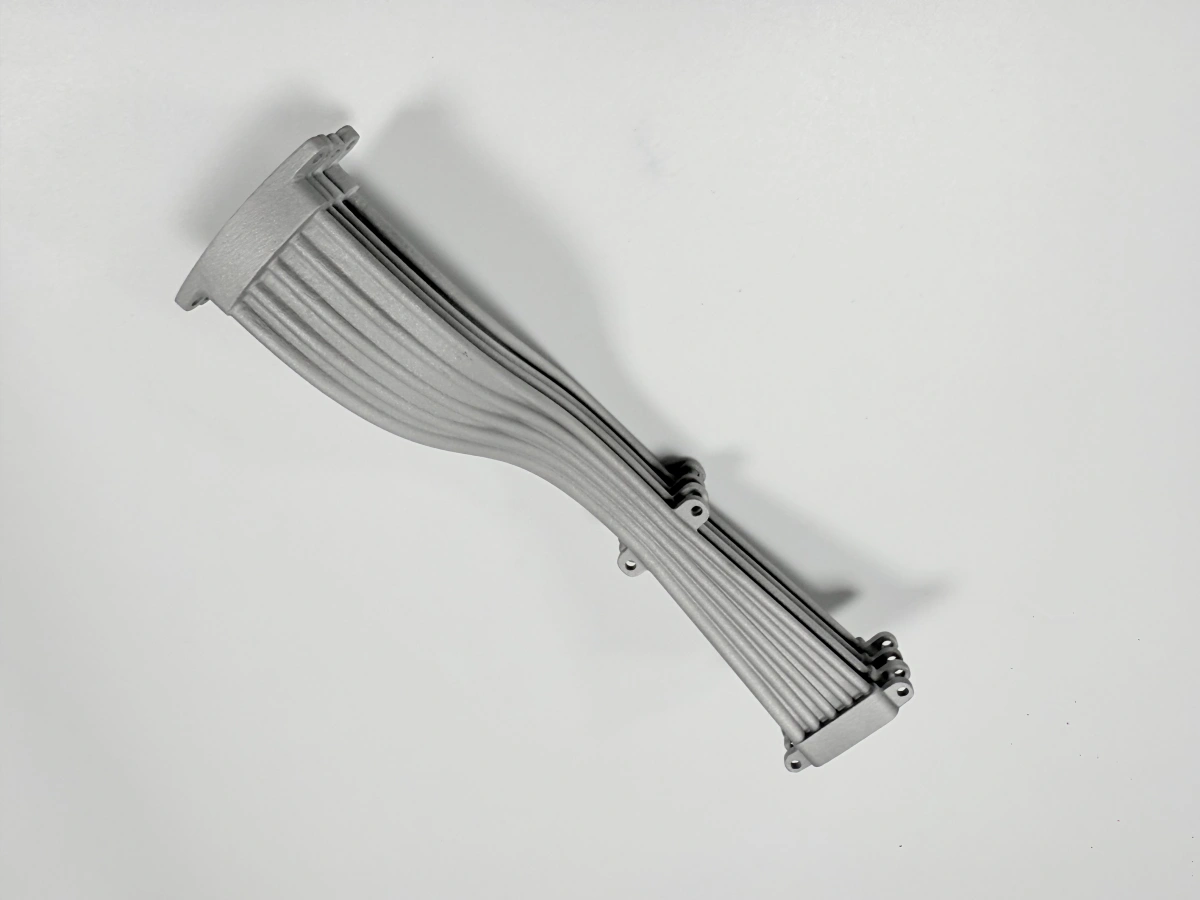
Additive manufacturing can integrate a manifold, reduce assembly count, or place material around a load path. That may improve system performance, but it also introduces powder-removal, inspection, support, and fatigue-detail requirements in aerospace or medical work.
For a fair comparison, test equivalent geometry and final condition. Compare load direction, surface preparation, thermal treatment, environmental exposure, and acceptance method. Record whether evidence comes from a standard coupon, a representative feature, or the production part.
Fatigue and Corrosion Resistance
Corrosion Resistance: Printed alloys retain chemistry-dependent behavior, but roughness, open pores, trapped powder, passivation, crevices, and the actual fluid can change the result. SUS316L should be assessed with a project-specific cleaning and corrosion method rather than selected from the grade name alone.
Fatigue Resistance: As-built stair steps, support scars, pores, and tensile residual stress can reduce life. Choosing surface treatments such as electropolishing may improve a specified surface, while HIP can address suitable internal pores. Specify stress ratio, load spectrum, orientation, surface condition, cycle target, and failure criterion.
Dimensional and Microstructural Control
Traditional machining starts from a known stock form and often provides predictable datums, while additive manufacturing creates a direction-dependent thermal history changed by stress relief, aging, HIP, machining, or coating. Verify chemistry and microstructure where required, inspect critical dimensions with CMM or a validated gauge, and use CT, penetrant, microscopy, or tensile testing according to the actual risk.
Summary Comparison Table
Feature | 3D Printed Stainless Steel | Traditionally Manufactured Stainless Steel |
|---|---|---|
Tensile Strength | Grade-, orientation-, and heat-treatment-specific; verify on agreed coupons or representative parts | Form-, grade-, and heat-treatment-specific; verify to the supplied specification |
Fatigue Resistance | Strongly affected by surface, defects, orientation, and HIP or finishing | Depends on material form, surface, load spectrum, and finish |
Corrosion Resistance | Alloy- and surface-condition-dependent; validate cleaning and exposure | Alloy-, surface-, and joining-condition-dependent; validate exposure |
Design Freedom | High for channels and consolidation, subject to access and inspection rules | Constrained by tool access, stock form, and assembly or joining strategy |
Lead time for low volume | Can avoid dedicated tooling; post-processing and approval still govern delivery | May require tooling, programming, setup, or supplier capacity |
Part Consolidation | Possible when powder removal, inspection, pressure testing, and repair access are solved | Usually uses separate parts or joining operations for enclosed functions |
Recommended Stainless Steel Printing Services
SUS316L: Evaluate for corrosion, cleaning, chemistry, surface, and fluid exposure.
SUS17-4PH: Evaluate aging condition, hardness, tensile direction, fatigue risk, and dimensional stability.
Heat Treatment: Specify the purpose; HIP: Verify the resulting condition, and do not treat either operation as proof that printed and wrought parts are automatically equivalent.
CNC Machining: Finish the interfaces that control fit, sealing, fatigue, or measurement.
.webp)