How does EDM precision compare to traditional machining methods?
How does EDM precision compare to traditional machining methods?
EDM and traditional cutting can both produce accurate parts, but their precision limits come from different error sources. EDM removes conductive material through controlled electrical discharges across a gap, so it avoids continuous cutter contact and can reduce force-induced deflection on hard or delicate features. Milling, turning, grinding, and honing use a tool or abrasive in contact with the workpiece; they can provide high accuracy when the part is stiff, accessible, and held correctly, but cutting force, tool wear, chatter, burrs, and access can become controlling risks. The right comparison is feature-specific and includes the printed starting state, tolerance, surface requirement, quantity, and final inspection.
Different Error Sources
In EDM, the programmed path is combined with spark gap, discharge stability, wire or electrode deflection, wear compensation, flushing, taper, recast, and thermal drift. In milling, the result also depends on spindle and tool runout, cutter deflection, tool wear, chip evacuation, chatter, fixture stiffness, and cutting parameters. Grinding can reduce roughness and control size, but wheel condition, dressing, heat, pressure, and access matter. A process with finer command resolution is not automatically more accurate on the completed printed part.
Printed metal adds another layer. Lack of fusion, gas porosity, residual stress, anisotropy, support-removal marks, and heat-treatment state can move the part when stock is removed or the fixture is released. EDM may avoid some mechanical force, yet electrical and thermal effects can still leave recast or a heat-affected zone. Conventional machining may be preferred for a stable external datum or large flat stock, while EDM may be preferred for a narrow slot, hardened cavity, or delicate conductive wall. A hybrid sequence is often more predictable than forcing one process to do every operation.
The precision mechanism also changes with the final pass. A lower-energy discharge can reduce crater size when the gap remains stable, while a cutting pass can leave burrs or deflection when force exceeds the printed wall's stiffness. Neither result should be inferred from the machine command alone; measure the same feature in the final condition and record the process that established its datum. A linked EDM process review should identify the gap, pass, and measurement condition used for the claim.
When EDM Is the Better Route
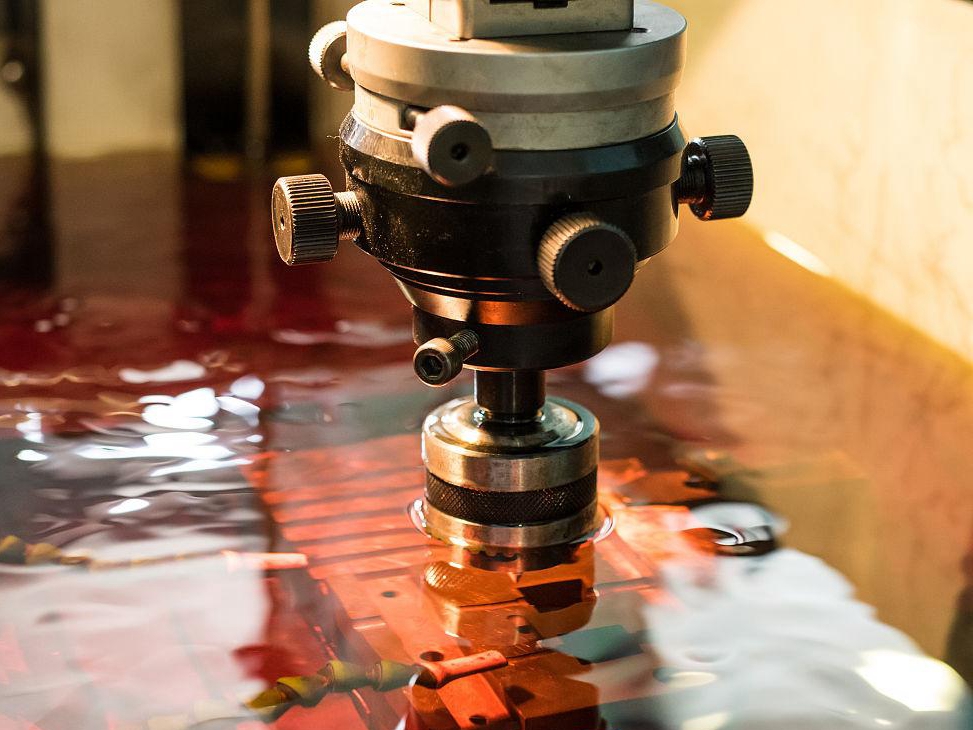
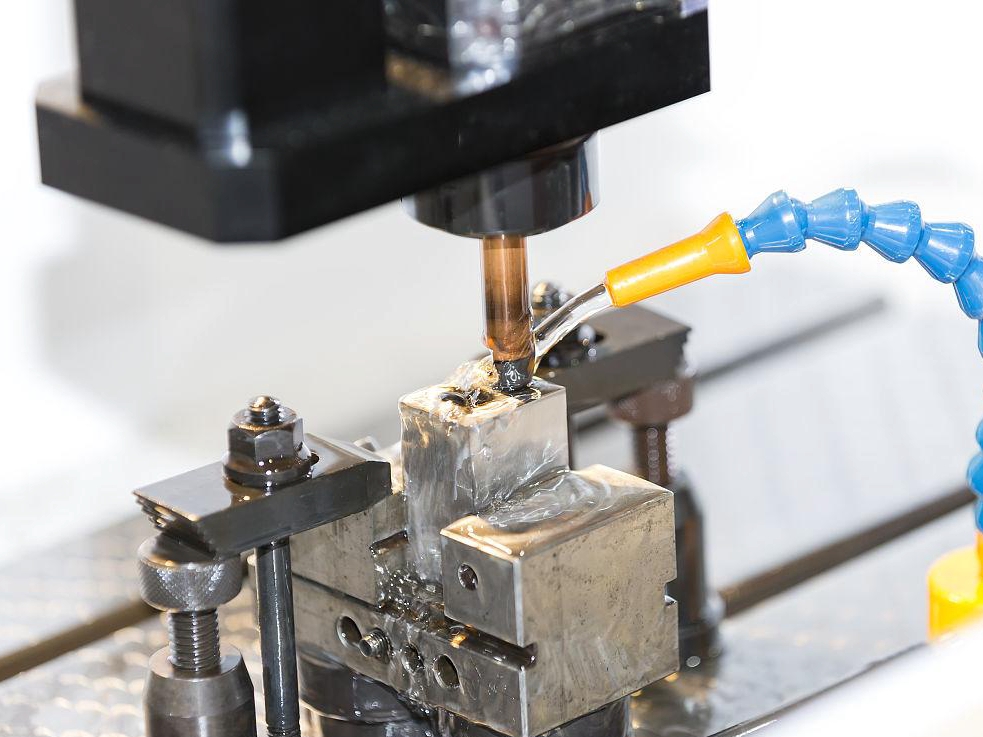
Choose wire EDM when a through-profile or start hole is available and the feature is conductive, hard, thin, or vulnerable to cutter force. The wire does not rub across the part, but wire tension, guide alignment, flushing, and support still affect a long contour. Choose sinker EDM when a shaped electrode can reach a blind cavity or local detail. The electrode must maintain form, debris must leave the gap, and corner transfer must be inspected. If the required feature is not electrically conductive or the tool cannot access it, EDM is not a precision solution simply because its machine display uses small increments.
Choose conventional milling or turning when the material is stable, the cutter has clear access, and force, tool wear, and chatter can be held within the drawing. Choose grinding or honing when a supported surface needs a controlled size and lower roughness after rough machining. Consider CNC machining as a complementary route for datums, open faces, and features better controlled by a cutting tool. The selection should identify which process establishes each critical dimension and which process performs the final verification.
Surface and Thermal Trade-Offs
EDM finishing can reduce crater size by using lower energy and stable flushing, but it does not remove material by abrasive smoothing. Recast and microcrack risk must be evaluated where fatigue, sealing, friction, or cleaning controls function. Milling can leave tool marks and burrs; grinding can create thermal damage or edge rounding; polishing can remove a critical allowance. A surface roughness value alone does not prove form accuracy, recast acceptability, or dimensional stability.
For a thin aerospace insert, EDM may be selected to limit cutting force, then the unclamped profile and surface integrity should be checked. For an automotive mold cavity, sinker EDM may establish a deep hard detail, followed by controlled polishing within a known allowance; inspect corners and final dimensions after the complete sequence. For a medical-development component, select the process only after the alloy, cleaning, sterilization exposure, and contact surface are defined. The process route should follow the risk being controlled, not a generic promise that EDM is universally more precise.
Comparison and RFQ Method
Ask for a comparison based on the same drawing revision, material lot, build orientation, heat-treatment condition, fixture datum, quantity, and final-state requirement. Request the expected tolerance, repeatability evidence, measurement instrument, temperature, roughness method, burr or recast limit, and disposition rule. If two processes are being compared, measure the same feature after the same cleaning and unclamping condition. A coupon is useful only when its stiffness, access, thermal state, and defect population represent the part.
For an aerospace fuel-injector contour, choose wire EDM when the through-profile and hard alloy make cutter force the main risk; verify profile, recast, and flow or leak performance. For a tooling cavity, choose sinker EDM when an electrode reaches the blind feature; verify corner form, roughness, and cavity dimensions after polishing. EDM can outperform contact machining for a particular risk, but the most accurate process is the one that produces the required final evidence on the actual geometry.
When comparing material capability, use the electrical discharge machining edm after the required property and section condition for this answer are fixed.
When planning the next process step, review the CNC machining service against the final geometry, inspection access, and release evidence described here.