What industries benefit from the application of TBCs on 3D printed parts?
What industries benefit from the application of TBCs on 3D printed parts?
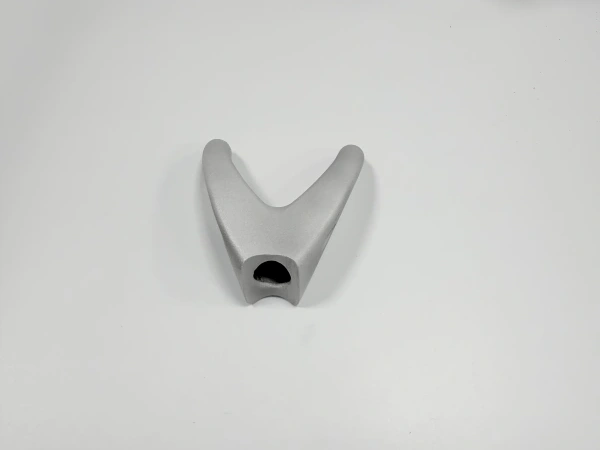
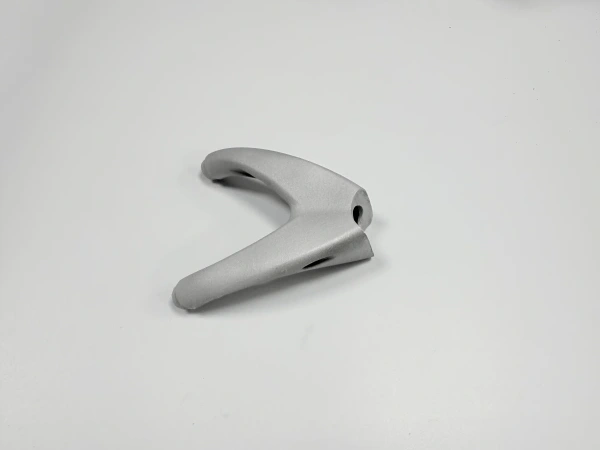
Industries benefit from TBCs on 3D-printed parts when the substrate temperature, thermal gradient, oxidation, or hot-environment damage is limiting and the coating system can be inspected on the actual geometry. Aerospace, power generation, automotive, marine, and chemical equipment may use TBCs, but each has a different heat flux, atmosphere, cooling route, vibration level, and qualification burden. Select a TBC from the failure mechanism and evidence plan, not from the industry label or a nominal ceramic temperature.
Aerospace and Power Generation
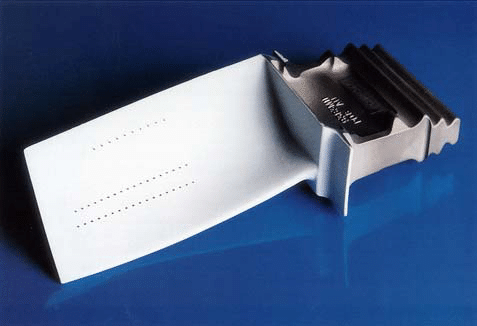
Aerospace hot-section brackets, combustor hardware, nozzle features, and thermal-management parts may use a TBC when the substrate metal is too hot under a defined gas temperature and cooling condition. The coating's ceramic topcoat adds thermal resistance, while the bond coat and TGO govern the interface. A rough printed surface, sharp corner, open pore, or orientation-dependent substrate can create a local failure site. Verify the critical feature's temperature, coating thickness, adhesion, thermal-cycle behavior, oxidation, and spallation. A flat coupon may support process knowledge but does not replace component inspection.
Power-generation hardware faces steady exposure and repeated starts and stops. A gas-turbine or heat-management part may benefit when heat flux and cooling flow are known, but the result also depends on erosion, salts, CMAS-like deposits, steam, and maintenance cleaning. Select the coating only when the bond coat and ceramic are compatible with the environment. Verify thermal response, TGO, interface condition, erosion, corrosion, and any pressure or flow function after exposure.
Automotive and Marine Equipment
Automotive exhaust, turbocharger, and engine-adjacent components can use TBCs to manage heat transfer when packaging, vibration, gas chemistry, and clearance are controlled. A coating that protects a hot wall may also change a seal fit, flow passage, or edge radius. Choose it when the thermal model or test identifies a substrate-temperature problem, then verify coating coverage, adhesion after vibration and thermal cycling, oxidation, erosion, and final dimensions. Do not assume that a coating rated for a static furnace is qualified for pulsating exhaust.
Marine hardware may combine heat with salt, humidity, vibration, and difficult maintenance access. A TBC may address heat transfer, but salt-driven hot corrosion and impact require separate evidence. Select the system only after defining the fluid, pressure, temperature, dwell, cycle, cleaning, and inspection access. Verify bond-coat condition, corrosion products, delamination, flow or leak performance, and the final coating state. A thermal barrier is not automatically a salt or wear barrier.
Chemical and Industrial Applications
Chemical processing equipment may experience hot gases, steam, reactive species, or salts. A TBC can reduce substrate temperature when the layer remains adherent, but chemical compatibility and permeability need separate evaluation. A porous ceramic may allow species to reach the bond coat; a crack can create a local attack path. For a printed manifold or reactor feature, verify channels, wall thickness, cleaning, pressure, leakage, and coating access. If corrosion resistance is the primary need, a compatible protective coating may be required in addition to the TBC.
Across industries, control the 3D-printed substrate before deposition. Record alloy, powder lot, build orientation, support removal, roughness, open defects, residual stress, and any heat treatment. Surface preparation under a qualified surface-treatment route affects adhesion and thickness. If internal porosity is the risk, evaluate it separately; a coating does not make a cracked substrate sound.
The accepted state must be the final coated 3D-printed part after any cleaning, thermal conditioning, or repair. A service label such as aerospace or automotive does not replace a temperature, adhesion, environmental, or dimensional criterion. State the coating architecture and final condition in the report so a buyer can distinguish the witness-coupon result from the delivered component.
Industry Evidence and RFQ
Build evidence around the application: thermocouple or validated thermal model for temperature, coating thickness map for coverage, ASTM C633 where suitable for adhesion, thermal-cycle exposure for spallation, and cross-section or NDT for interface condition. State heat flux, gas temperature, cooling, ramp, dwell, atmosphere, cycles, sensor location, resolution, uncertainty, and acceptance limit. For a production quote, provide drawing revision, material and lot, geometry, surface state, coating system, environment, inspection, quantity, and approval authority. Release the final coated part only when the industry-specific function and coating integrity are both demonstrated.
If this question concerns a failure mechanism, compare the thermal barrier coating service after the suspected cause and test condition are identified.
For a controlled production decision, request the surface-treatment service when the final state and deviation path need traceable evidence.