How do TBC coatings improve engine efficiency and performance?
How do TBC coatings improve engine efficiency and performance?
A TBC may support engine efficiency or performance when it reduces the heat reaching a defined substrate or manages a specified hot-surface temperature under the actual gas, cooling, pressure, vibration, and maintenance conditions. A cooler substrate can support a thermal design objective, but the coating does not automatically increase engine output or fuel efficiency. The result depends on heat flux, coating thickness and structure, bond-coat condition, gas chemistry, cooling flow, thermal cycle, erosion, and the final geometry. Separate a thermal measurement from an engine-level performance claim.
Heat Flow and Thermal Boundary
Heat passes from combustion gas to the coating surface, through the ceramic topcoat and bond coat, and into the printed metal. Under a defined heat flux and cooling route, added thermal resistance may lower the interface or substrate temperature. The benefit depends on conductivity, porosity, thickness, contact resistance, gas velocity, cooling-hole behavior, ramp, and dwell. State whether the value is gas, surface, interface, or metal temperature. A static furnace coupon cannot replace a representative engine thermal test.
The performance boundary includes the interface. The metal, bond coat, TGO, and ceramic expand differently during starts, stops, and load changes. Mismatch strain may initiate microcracks or delamination. Particles can erode the topcoat; salts and deposits can drive hot corrosion or CMAS-like damage. A TBC can improve a thermal input condition while reducing performance if spallation changes clearance, blocks a passage, or exposes the substrate. Define the engine function and failure criterion together.
Printed Geometry and Final Condition
Thin printed walls, cooling channels, sharp edges, and rough surfaces produce nonuniform heat flow and coating access. Inspect the substrate for particles, pores, cracks, residual stress, and support marks. Record alloy, lot, orientation, section thickness, and any heat treatment, HIP, machining, or surface treatment. The final coated state is the release state; it is not interchangeable with the as-built or coupon state. Recheck seals, holes, datums, and clearances after coating.
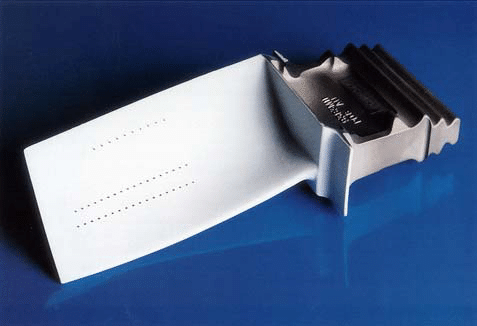
The engine-level process has to preserve function. If coating changes a cooling-hole diameter, channel roughness, seal clearance, or edge radius, the thermal benefit cannot be evaluated separately from the functional change. Measure the final condition after deposition and any conditioning. Use a pressure, flow, or leakage test where the feature carries fluid, and use a thermal-cycle inspection where temperature or strain is the concern.
Do not convert a local temperature result into an engine-efficiency promise without system evidence. Under a defined boundary condition, the coating may support a thermal design target. The engine outcome still depends on gas flow, cooling, combustion, pressure loss, vibration, deposits, and maintenance. Record which variable was measured and which variables remain unverified.
Validation and RFQ Decision
For a turbine bracket, choose a TBC when substrate temperature is limiting and verify temperature, thickness, adhesion, cycles, TGO, spallation, and fatigue separately. For an exhaust component, include pulsating heat, vibration, erosion, and gas chemistry. Use calibrated thermal measurement, representative cycling, thickness mapping, adhesion testing when suitable, and final dimensional or flow inspection. Provide CAD revision, alloy and lot, geometry, heat flux, temperatures, cooling, cycle, coating system, thickness, inspection, quantity, and approval authority. Request deposition records and release the engine claim only for the tested final condition.
Industry Fit and Acceptance
Industry selection should start with the failure mechanism and the inspection route. Define the substrate grade, coating architecture, operating atmosphere, temperature history, cooling method, critical geometry, access for inspection, and acceptance limit. Use representative coupons only to screen a route; qualify the final printed part when thermal gradients, edges, holes, or thin walls control the risk. Request thickness maps, adhesion results, thermal-cycle records, and a disposition for any damaged area.
Before approving this application route, check the thermal barrier coating service against the part's operating condition, critical feature, and acceptance limit.
For supplier comparison, use the heat-treatment service to separate a process capability statement from evidence on the completed part.