How does HIP improve surface finish compared to traditional polishing methods?
How does HIP improve surface finish compared to traditional polishing methods?
HIP and polishing act on different parts of a 3D-printed component. HIP uses heat and isostatic gas pressure to reduce suitable closed internal porosity only when the pore is isolated and the material cycle is qualified. Polishing, machining, abrasive flow, or electropolishing removes or levels material at an exposed surface. HIP can support a smoother and more reliable final surface only when subsurface pores would otherwise open during machining or service, but it does not automatically remove layer texture, support scars, adhered powder, or a surface-connected crack. Select the route from the actual defect, the functional surface, and the final measurement method.
Different Mechanisms
The two routes should be separated in the process traveler because they change different failure variables. HIP is a heat treatment that addresses internal porosity and the material state under a qualified pressure-temperature cycle; polishing addresses the exposed profile and edge condition. If a subsurface pore later opens during machining, HIP may support the finishing route, but the surface result still depends on stock removal and the final measurement. If the surface is already acceptable but fatigue evidence is missing, polishing alone does not answer the internal-defect question.
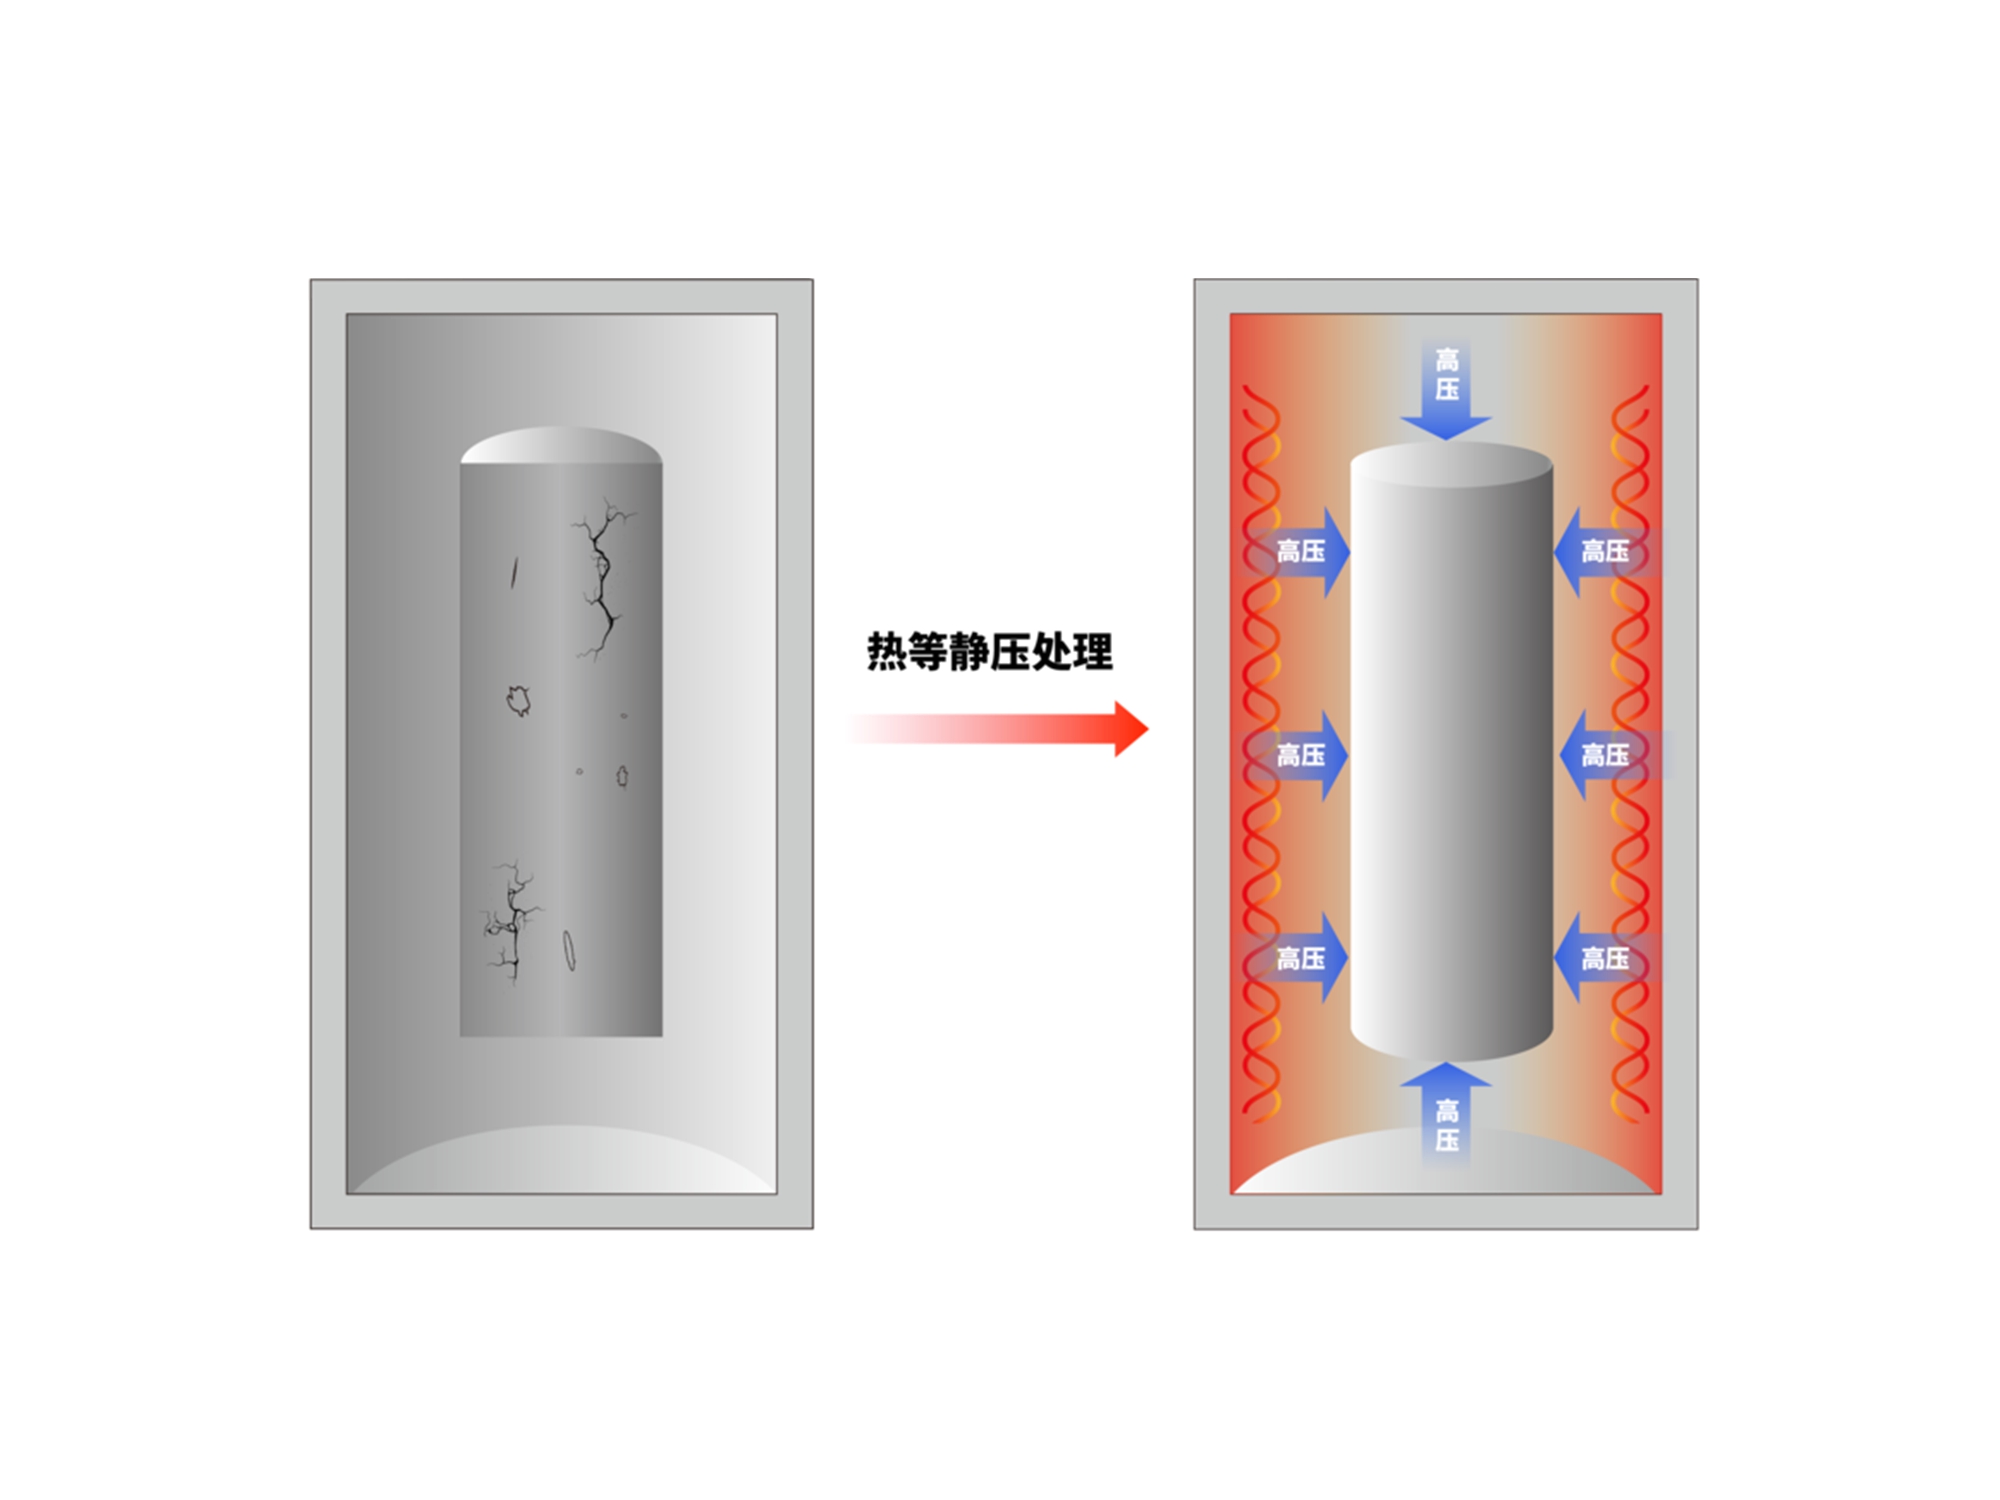
HIP changes the internal material state only when the material, atmosphere, pressure, temperature, hold, and cooling path are qualified, because temperature increases creep and diffusion while gas pressure applies compressive stress around the part. A closed pore may shrink and bond under that qualified cycle. That response can reduce a hidden source of pits or premature fatigue only when the pore is the controlling defect and the result is verified after machining. It does not provide cutting action at an exposed peak. A rough surface caused by layer geometry remains rough unless a later operation changes its profile.
Traditional polishing works by controlled material removal or redistribution at the surface only when the selected media, pressure, chemistry, and stock are controlled. Machining establishes a datum and can remove a defined depth; abrasive finishing reduces peaks but can round edges; electropolishing removes material according to the electrical and chemical condition; coating adds a new surface and introduces an interface. Each route changes dimensions and edge condition differently. The correct comparison therefore records Ra or another agreed metric, waviness, form, feature size, and the state in which the part is measured. A visual impression is not enough for a seal, bearing, flow, or fatigue claim. This separation matters because internal porosity and final material state can influence service even when two surfaces have similar profile values.
When HIP Helps a Surface Route
For a machined Inconel 718 bracket, HIP may be selected before final machining when internal porosity is a credible fatigue origin and there is enough stock to absorb dimensional movement. The buyer should verify CT or metallography before and after, final dimensions, surface roughness after machining, and representative fatigue if specified. If the measured roughness fails after machining, add a finishing operation or revise the surface route; do not describe HIP as a replacement for polishing.
For a powder-bed part that receives HIP and heat treatment, report the surface result only after the final treatment and final state are established. The later thermal step can change hardness, oxidation, or dimensional response, while machining can remove the roughness that was present immediately after HIP. Keep the operation sequence, specimen identity, surface direction, and measurement locations fixed. If the comparison cannot isolate HIP from polishing or heat treatment, label it as a combined route and keep the single-process claim unproven.
For a 316L pressure manifold, HIP may be selected when a closed pore could form a leak path after machining. The surface route still requires cleaning, access review, roughness measurement where flow or sealing depends on it, and a pressure leak test at stated medium, pressure, temperature, and dwell. For a tool-steel insert, HIP may support cavity integrity before hardening and polishing, but the cavity profile, hardness, corner condition, and polishability remain separate release checks.
Comparison Evidence
Use matched samples when comparing HIP with a polishing route. Hold the material lot, build orientation, section, surface preparation, machining allowance, and final thermal condition constant. Measure the same locations and directions before treatment, after HIP, after rough machining, and after final finishing. If one group is polished and the other is only HIP-treated, report a combined process comparison rather than an HIP-only effect. ISO 21920 may provide a profile-reporting framework when invoked by the project, but it does not set a universal acceptable Ra for every part.
Pair roughness with the measurement that controls function only when the method can observe the accepted feature. A profilometer can describe a sampled external trace but may not reach a deep channel. CT can show internal indications and geometry but does not directly prove a surface profile at every location. A leak test can demonstrate pressure-boundary performance under its stated condition but cannot establish polish quality. State resolution, sampling, uncertainty, orientation, test condition, and acceptance limit in the report. If the surface measurement and functional test disagree, hold the part for engineering review.
Buyer Choice and RFQ
Choose HIP before polishing when the defect is internal, closed, measurable, and relevant to the service risk. Choose machining or polishing when the requirement is an external profile, datum, seal land, or appearance. Choose a combined route when both conditions exist. Provide drawing revision, grade and lot, additive process, orientation, pore evidence, critical surface, initial and target roughness, waviness or form limits, stock, cycle, finishing operation, inspection method, quantity, and acceptance authority. Request the cycle record, dimensional map, before-and-after internal evidence, final surface report, and deviations. The supported result is the final measured condition, not the name of the HIP process.
For a primary route decision, use the HIP processing service after the material, geometry, and service condition for this question are defined.
For downstream verification, consult the surface-treatment service when the final process state and acceptance evidence for this question must be recorded.
.webp)