
How does HIP enhance fatigue resistance in aerospace components?
How does HIP enhance fatigue resistance in aerospace components?
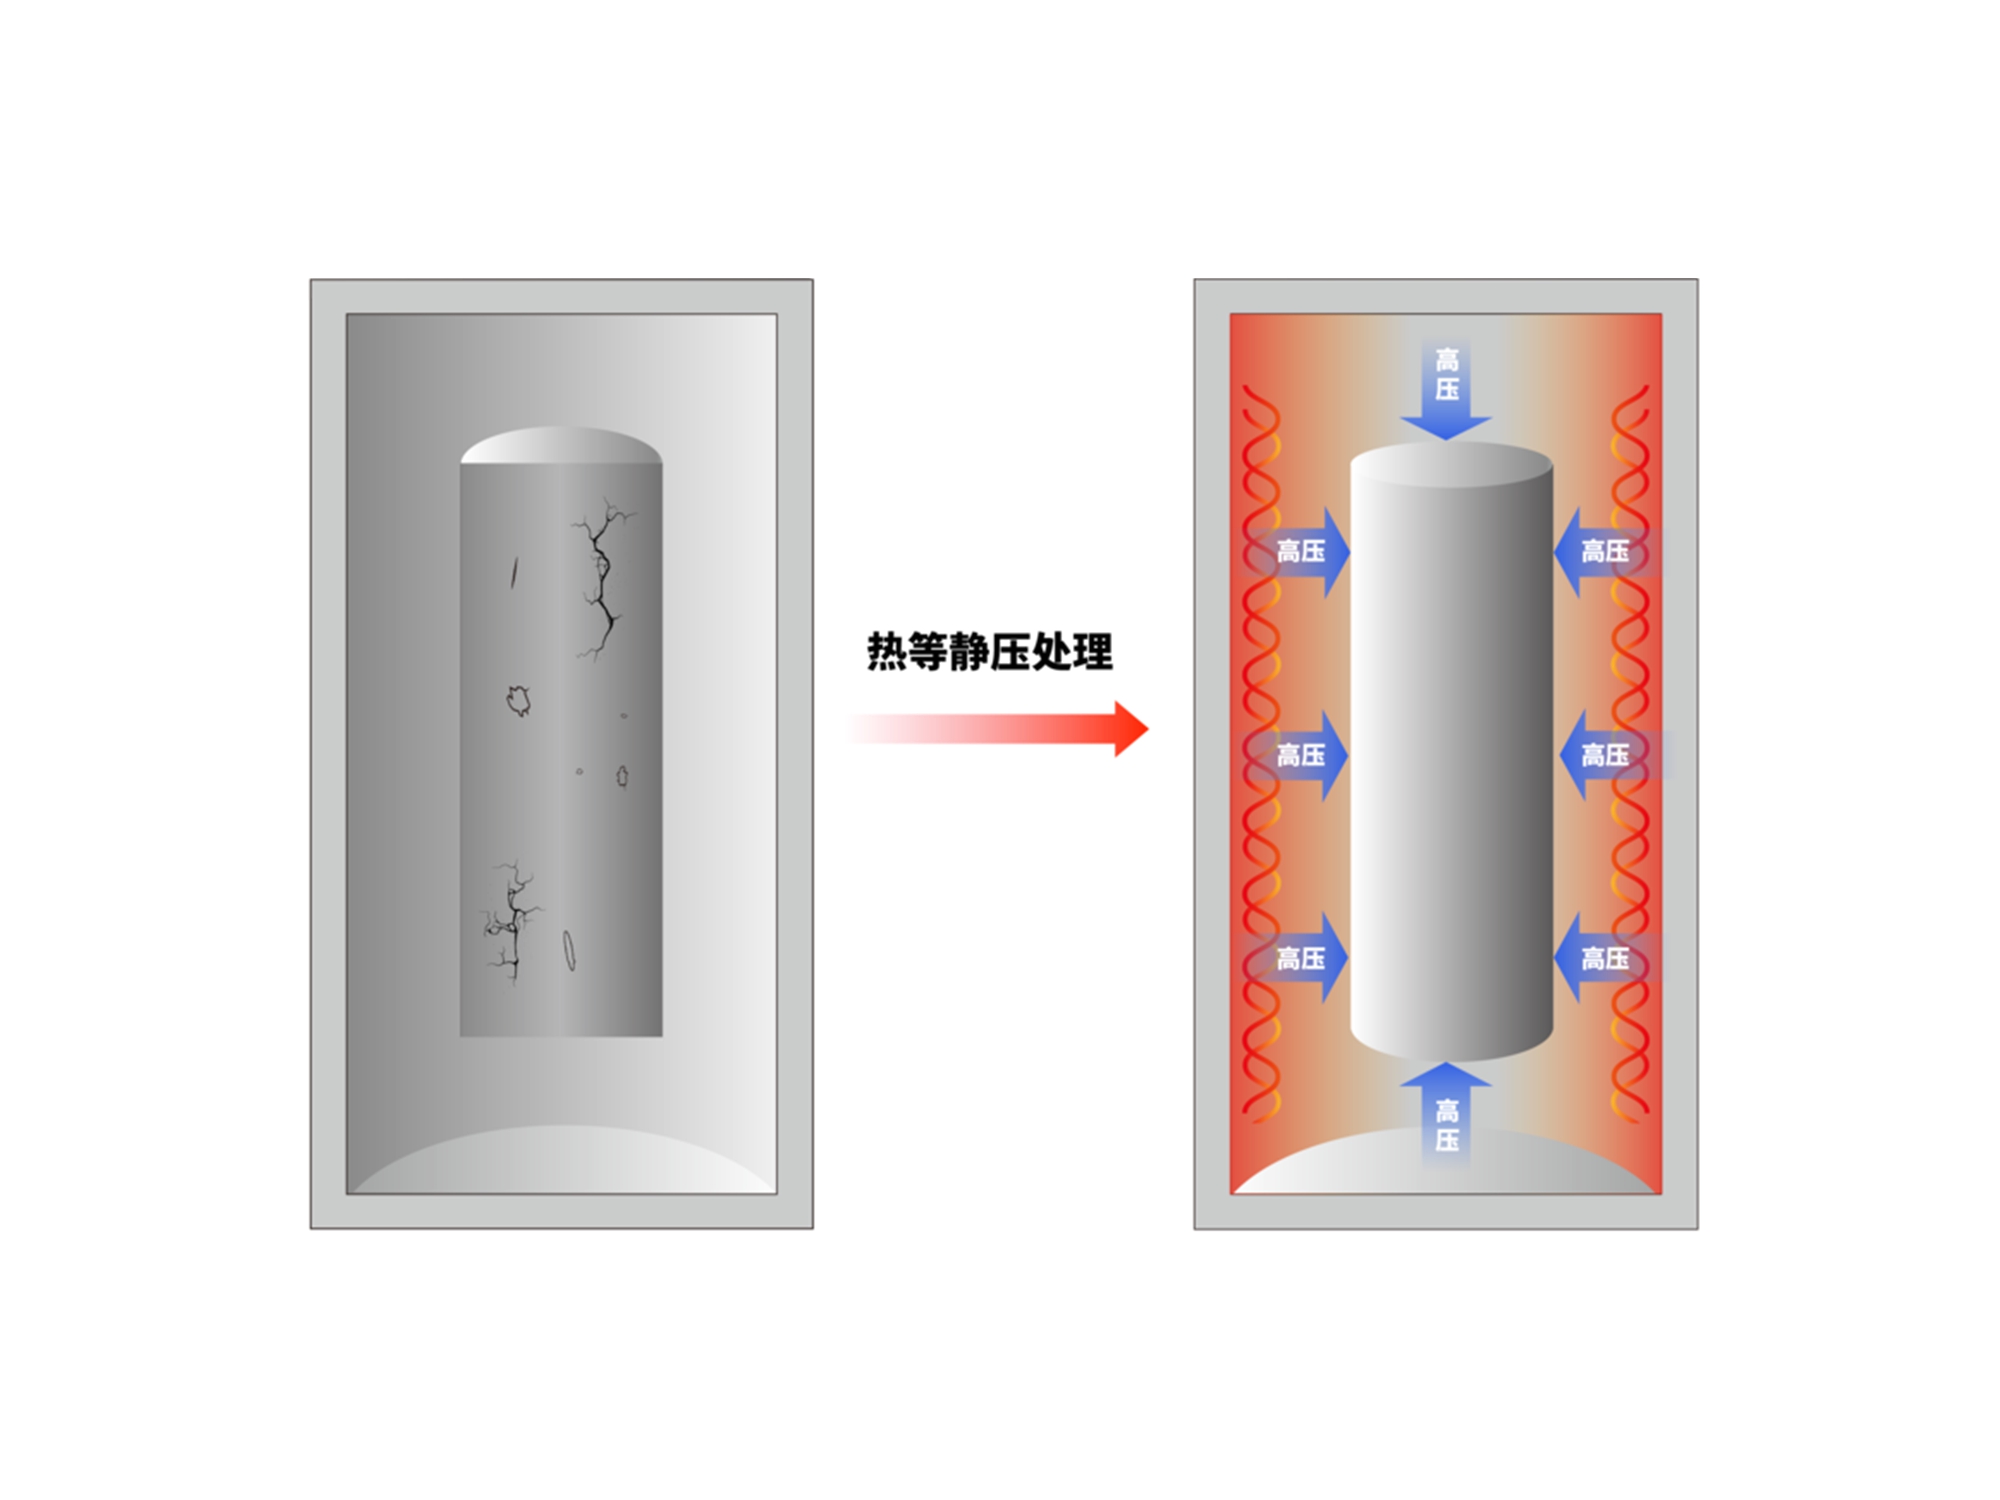
HIP can support aerospace fatigue resistance when a suitable closed internal pore is a credible crack origin and the material cycle, surface state, geometry, and evidence plan are qualified. Fatigue is controlled by more than bulk density. Build orientation, surface roughness, lack of fusion, inclusions, residual stress, alloy condition, temperature, stress ratio, and load spectrum can all matter. HIP combines heat and isostatic pressure to reduce some internal voids; it does not automatically repair a surface crack or establish airworthiness.
Fatigue Mechanism
A pore can reduce load-bearing area and amplify local stress. Under cyclic loading, a crack may initiate at the pore and grow through the component. If the pore is isolated and responds to the qualified cycle, HIP may reduce that initiation site because surrounding material moves inward and can bond. The result depends on pore morphology, alloy chemistry, pressure, temperature, hold, cooling, and subsequent heat treatment. If fracture begins at a rough surface, lack of fusion, notch, or machining mark, internal densification may not control the result.
Inconel 718 needs a defined precipitation condition after HIP, while Inconel 625 uses a different strengthening basis. Ti-6Al-4V requires orientation, alpha-beta morphology, oxygen control, and surface review. A polished fatigue coupon may show a different result from an as-built bracket with a machined bore. Keep the HIP cycle, later aging, machining, and surface condition separate in the traveler and in the fatigue report.
Fatigue evidence must connect the process route to the aircraft component's actual risk. A coupon can show how the alloy and cycle behave, but its surface, geometry, orientation, and stress concentration may differ from a bracket, housing, or manifold. Record whether the specimen was as-built, machined, polished, heat treated, or coated. If HIP is combined with solution treatment and aging, label the combined condition. If the component has a surface-connected indication or the CT resolution cannot resolve the critical section, obtain another inspection method or engineering disposition.
For a hot-section bracket, select HIP when a closed pore is mapped near the fatigue-critical section and the final Inconel 718 precipitation condition is specified; verify CT, dimensions, roughness, hardness or tensile state, and representative fatigue or creep. For a titanium actuator housing, choose it when internal indications are linked to cyclic loading; verify oxygen record, orientation, heat treatment, bore geometry, and fatigue. For a pressure manifold, choose it when the pore risk is demonstrated and pair fatigue evidence with wall-thickness and leak testing.
Aerospace Test Evidence
Use ASTM E466 for axial fatigue when its specimen and loading scope fit the project, and state orientation, surface preparation, stress ratio, frequency, temperature, runout, sample count, and acceptance rule. Use CT or metallography to characterize internal indications and record resolution and threshold. Analyze fracture origins rather than reporting only average cycles. For a component, define the critical section, load spectrum, surface state, dimensions, and inspection authority. A coupon result supports process knowledge but does not replace component evidence.
Compare HIP-treated and reference material with the same alloy lot, build parameters, orientation, geometry, surface preparation, machining, heat treatment, and test condition. If HIP is combined with solution treatment and aging, identify the combined condition. If the reference contains a different surface notch or orientation, the comparison cannot isolate the HIP effect. When an indication is surface-connected or the CT resolution is insufficient, obtain a complementary method and engineering disposition before crediting fatigue improvement.
Component Scenarios
For an Inconel 718 hot-section bracket, select HIP when closed porosity is mapped near a fatigue-critical section and the post-HIP precipitation condition is defined. Verify CT, free-state dimensions, final roughness, hardness or tensile condition, and representative fatigue or creep. For a titanium actuator housing, select it when internal indications are linked to cyclic loading; verify orientation, oxygen record, heat treatment, surface, bore geometry, and fatigue. For a pressure-containing aerospace manifold, pair internal inspection with wall thickness and leak evidence.
RFQ and Release Boundary
Provide drawing revision, alloy and lot, additive route, orientation, section thickness, defect map, surface state, load spectrum, temperature, target fatigue criterion, HIP pressure and temperature, hold, cooling, later heat treatment, machining allowance, CT or metallography resolution, fatigue method, sample count, quantity, and approval authority. Request cycle records, calibration, internal evidence, dimensional maps, surface data, mechanical results, fracture analysis, and deviations. HIP may support a fatigue claim only when the final measured evidence supports it; it does not create aerospace qualification by itself.
For RFQ preparation, request the HIP processing service after the buyer defines the material state, quantity, and required verification method.
For final release, compare the heat-treatment service with the inspection record, service condition, and disposition of any unresolved risk.
.webp)
