Does HIP affect the dimensional accuracy of the part during densification?
Does HIP affect the dimensional accuracy of the part during densification?
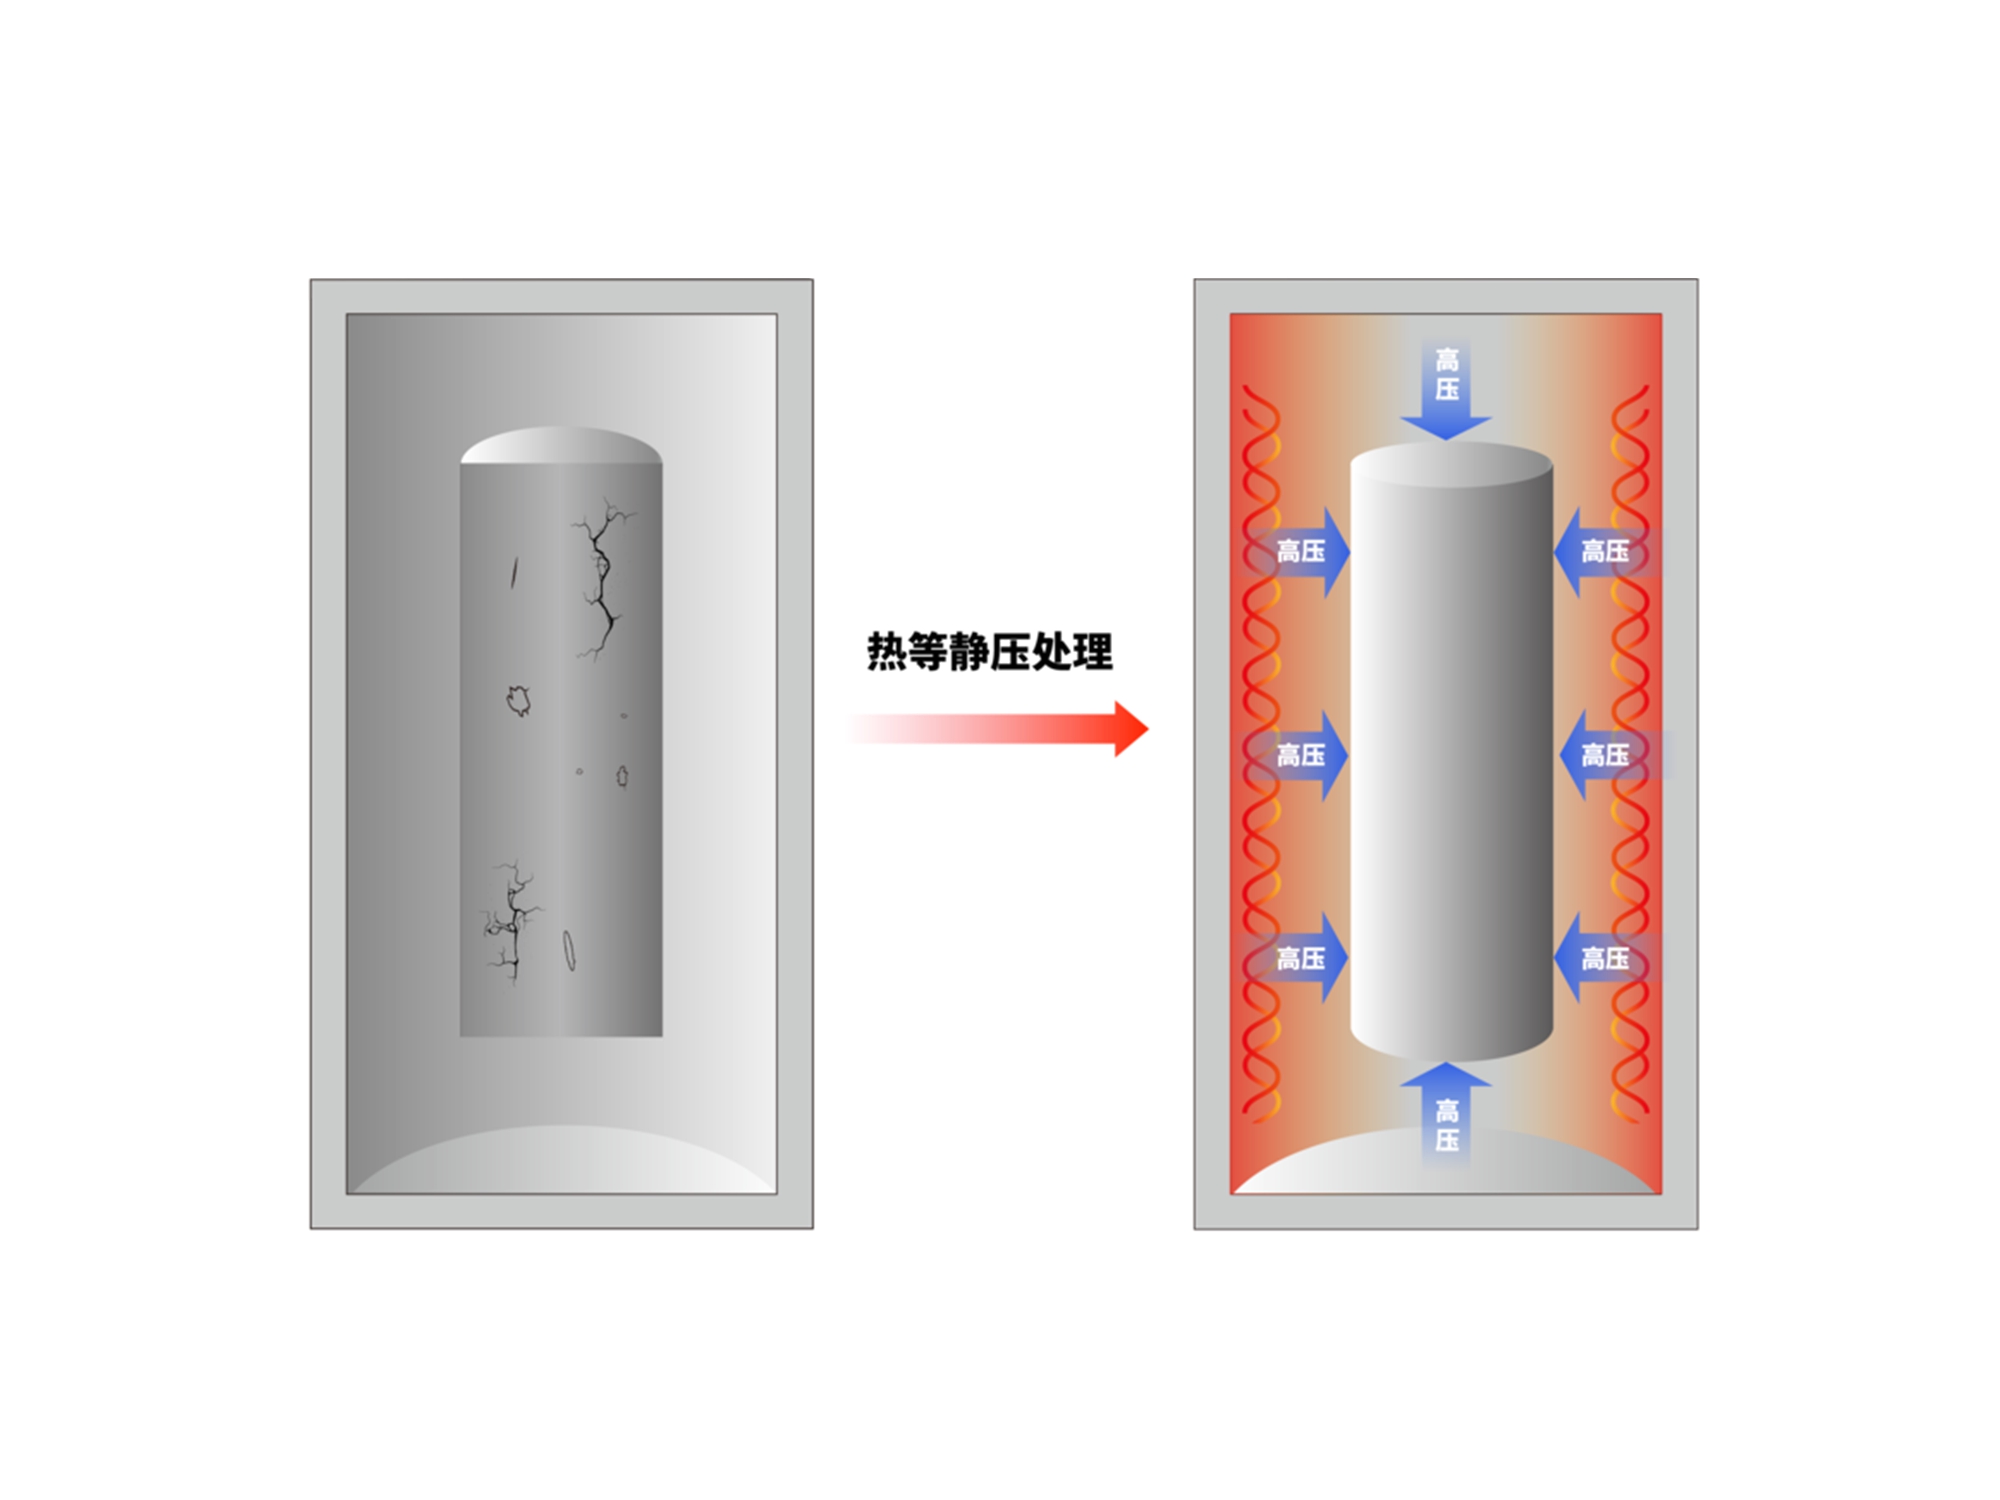
HIP can affect dimensional accuracy because the combined temperature and pressure may cause creep, shrinkage, pore closure, phase change, or release of residual stress. The amount and direction depend on alloy or ceramic composition, porosity, section thickness, geometry, build restraint, fixture, load position, and cooling. A nominally isostatic pressure does not guarantee uniform dimensional change in a complex component. Measure critical datums before and after HIP in a free, defined state, and verify the final result after machining when that operation changes the accepted feature. The final dimensional decision is valid only when the measurement method, uncertainty, and acceptance limit are stated; it is project-specific and not established by a nominal vessel setting alone.
For a dimensional claim, define the state being compared: attached to the plate, support-removed, cleaned, HIP-cooled, unclamped, rough-machined, or final-machined. Record the same datum reference, inspection temperature, instrument, uncertainty, and sampling points at each state. If the measured change is smaller than the method uncertainty, report it as unresolved rather than as proof of zero movement. If the change exceeds the drawing tolerance but machining stock can recover it, verify the final feature after machining; if stock cannot recover it, hold the part.
Sources of Movement
Closed pores can collapse locally, changing a wall or surface profile. Thin and thick sections reach temperature at different times, which creates transient gradients. Residual stress can redistribute as the material is heated, and prior support removal can release strain before the cycle. A fixture may protect one datum only when its contact and restraint direction are qualified for the load; it can impose a force on another because the constraint changes the free deformation path. Ceramics add green-body and firing shrinkage considerations; their dimensional plan must include the full fired state rather than only HIP.
Movement is especially consequential when a pressure channel, bearing bore, seal land, or optical datum has little corrective stock. A local pore closure may change a thin wall without producing a visible change in the outside envelope. A constrained fixture can make the in-process measurement look stable while the feature moves after unloading. Inspect the functional feature in its release condition and record fixture contact points so the result can be reproduced.
Dimensional movement is a release risk when the accepted feature is near the available machining allowance. Compare the measured change with the drawing tolerance, stock, and instrument uncertainty, then verify the final part after machining. If a scan shows a shift but the measurement setup was different, repeat the inspection before changing the process. A qualified dimensional conclusion requires a defined free-state condition and a stated disposition rule.
Geometry controls the inspection problem only when the selected method can access the accepted feature. Deep channels, lattices, sharp corners, and thin flanges may not be accessible to a stylus. A clamped scan can hide free-state movement, and a surface measurement cannot prove an internal bore. Define whether the part is attached, support-removed, clamped, unclamped, rough-machined, finished, or coated. Use a CMM, scan, CT, gauge, replica, or flow method that can observe the accepted feature.
Sequence and Machining Allowance
Plan the sequence from the build state through cleaning, HIP treatment, heat treatment, rough machining, finishing, and inspection. Capture a pre-HIP map with stable datums, then repeat the map after cooling and release. If final dimensions are established by CNC machining, reserve allowance based on measured movement rather than a generic value. HIP cannot correct a misplaced feature beyond the available stock, and excessive stock removal may change wall thickness or balance.
Verification
Use the same measurement temperature, coordinate system, datum sequence, sampling points, instrument, and uncertainty before and after HIP. For a precision ring, inspect bore position, roundness, and concentricity after the final cut. For a pressure manifold, inspect channel position, wall thickness, leak performance, and surface condition. For a conformal-cooling insert, map cavity datums, channel leakage, hardness, and polish allowance. If a witness coupon is used, match section and restraint; a simple coupon cannot prove complex geometry.
Use CT when internal geometry and resolution support the claim, or use a validated flow, gauge, or replica method when it is more appropriate. Keep surface finishing separate because blasting, polishing, coating, or machining can change dimensions and roughness after HIP. Inspect after the last dimension-changing operation. If a feature passes before HIP but fails afterward, hold the part for engineering disposition rather than assuming the result is normal densification.
For a thin flange, compare profile and fastener-hole position before and after support removal and again after HIP. For a deep conformal channel, combine CT or a validated replica with wall-thickness and flow evidence because flow alone may miss a local restriction. For a precision bore, inspect roundness and concentricity after the final cut with the part free of clamping force. Each method must state what it can and cannot prove, and each failed result needs a defined rework or engineering-disposition path.
RFQ and Release
Provide CAD and drawing revision, material and lot, additive route, orientation, section, critical datums, tolerance budget, defect evidence, HIP cycle, loading, fixture, cooling, prior heat treatment, machining allowance, surface, inspection method, quantity, and acceptance authority. Request pre- and post-HIP dimensional maps, CT or metallography, cycle records, calibration, final dimensions, and deviations. HIP does not guarantee dimensional accuracy or establish pressure, aerospace, or medical qualification. Release only the final measured condition.
Before approving this application route, check the HIP processing service against the part's operating condition, critical feature, and acceptance limit.
For supplier comparison, use the heat-treatment service to separate a process capability statement from evidence on the completed part.
.webp)