Can HIP effectively smooth internal surfaces or complex geometries?
Can HIP effectively smooth internal surfaces or complex geometries?
HIP should not be selected as a general method for smoothing internal surfaces or complex geometries. It may reduce suitable closed porosity within the material, but it does not guarantee a smooth channel wall, remove trapped powder, erase support residue, correct a constricted passage, or polish a lattice. Internal surface acceptance depends on access, material state, geometry, cleaning, measurement resolution, and the functional test. Define the internal claim before choosing a thermal or finishing route.
Internal Surface Mechanism
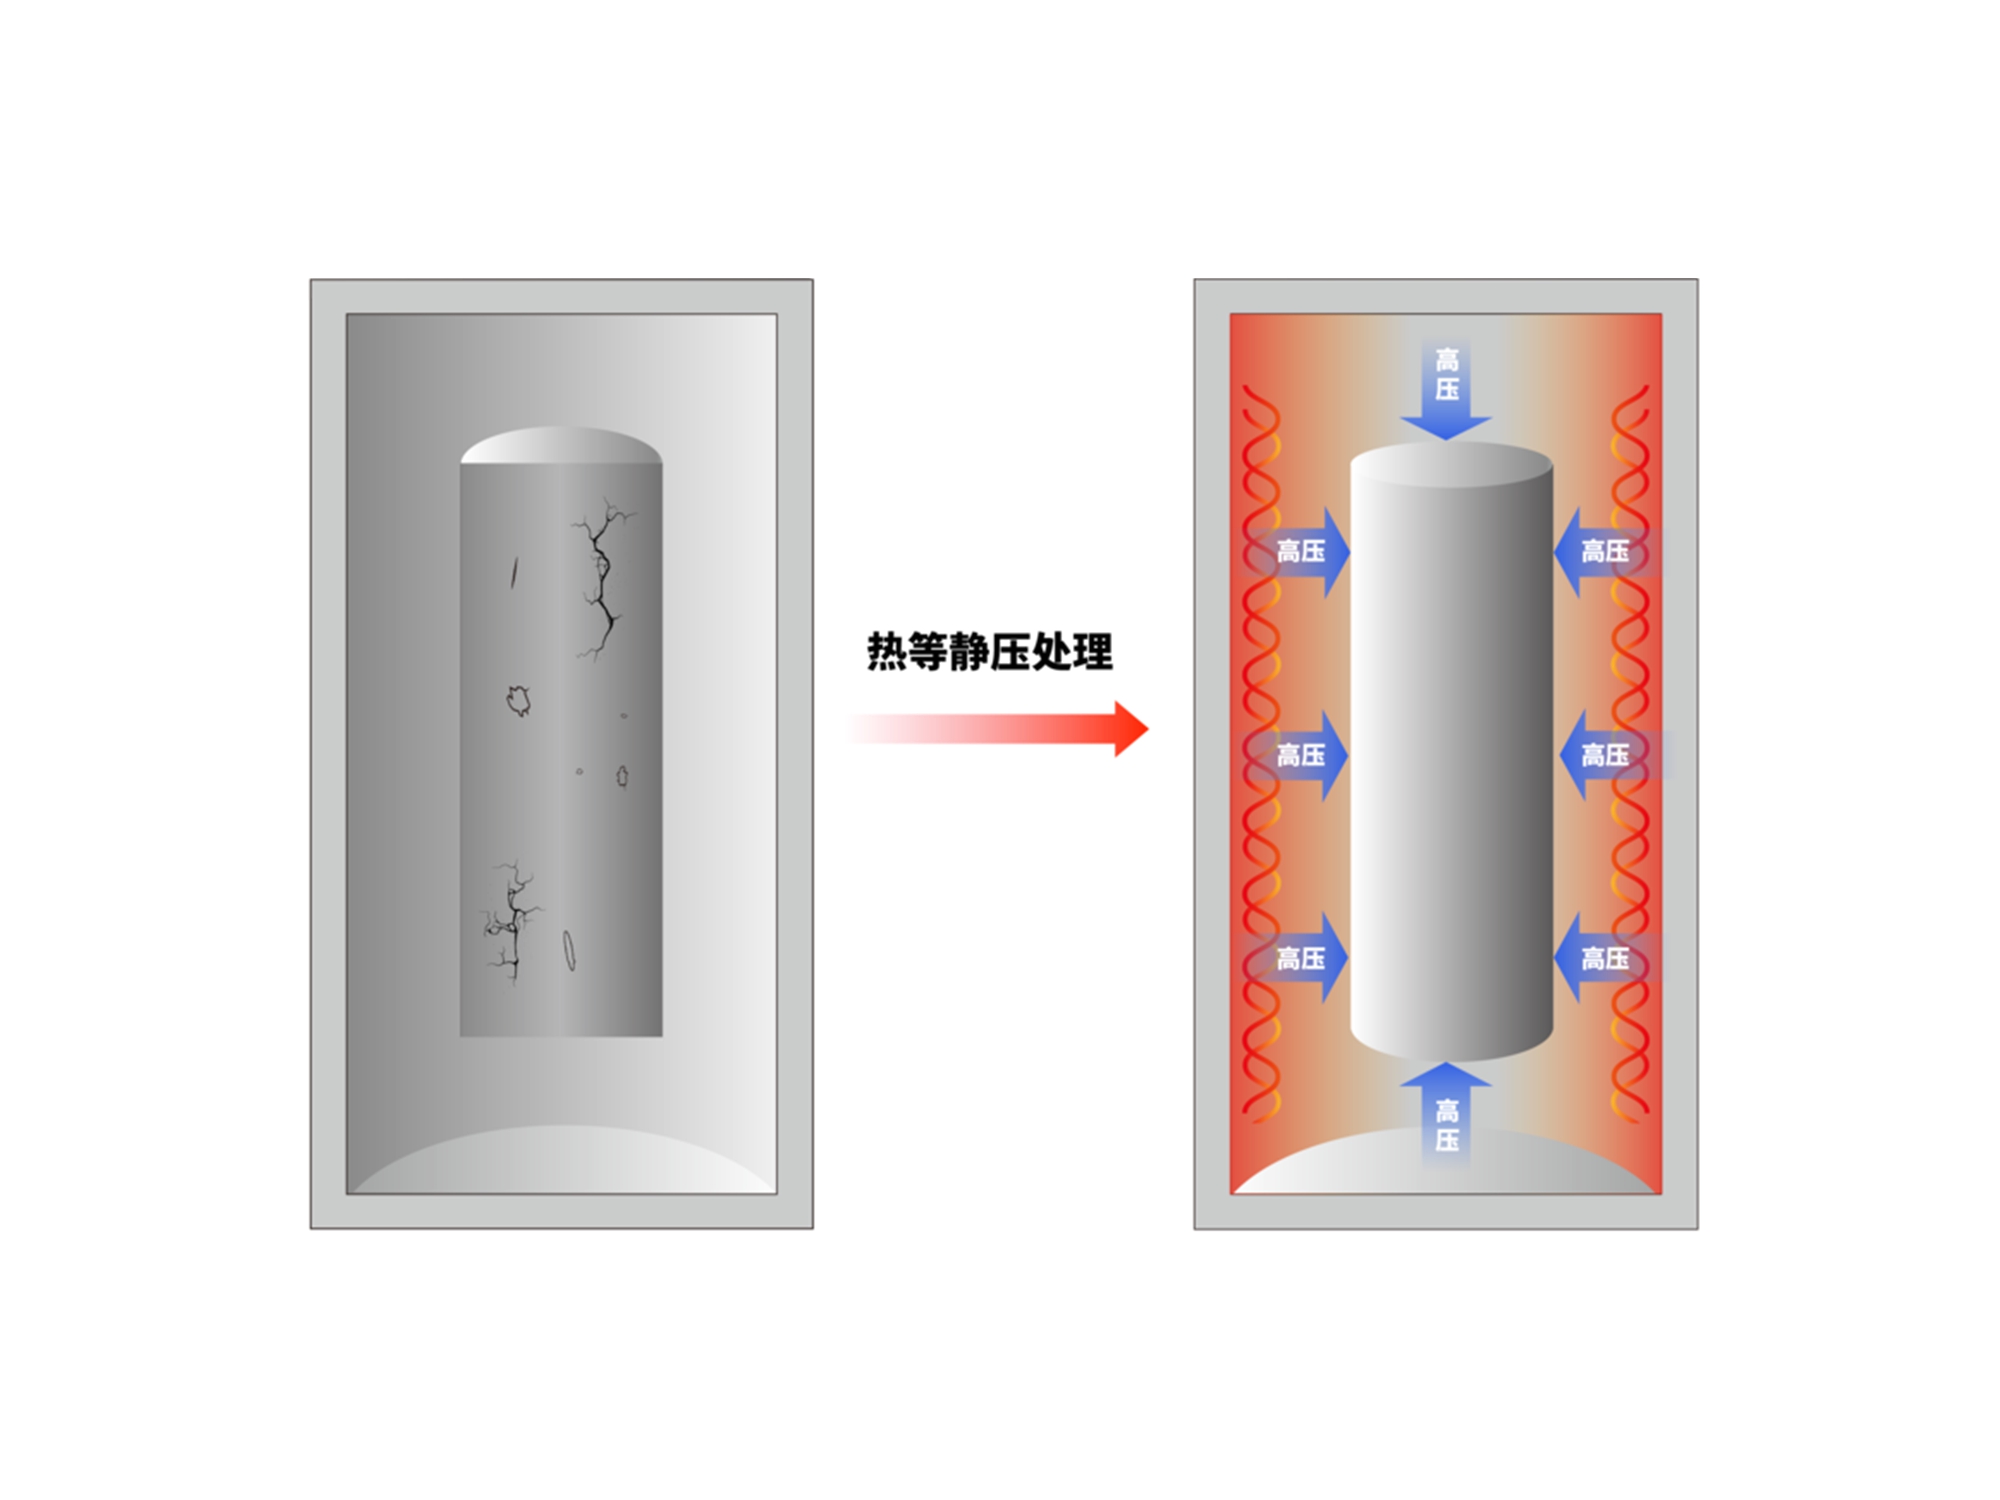
Within a closed pore, heat and isostatic pressure can promote creep and diffusion because the surrounding material is able to move toward the void. This mechanism may improve the internal integrity of a thick wall when the pore is isolated and the cycle is qualified. It is not a surface-level smoothing action. A rough channel wall created by layer stacking remains rough unless a finishing method reaches it. A surface-connected crack or open pore can remain a release issue, and contamination can remain trapped if the route cannot clean it.
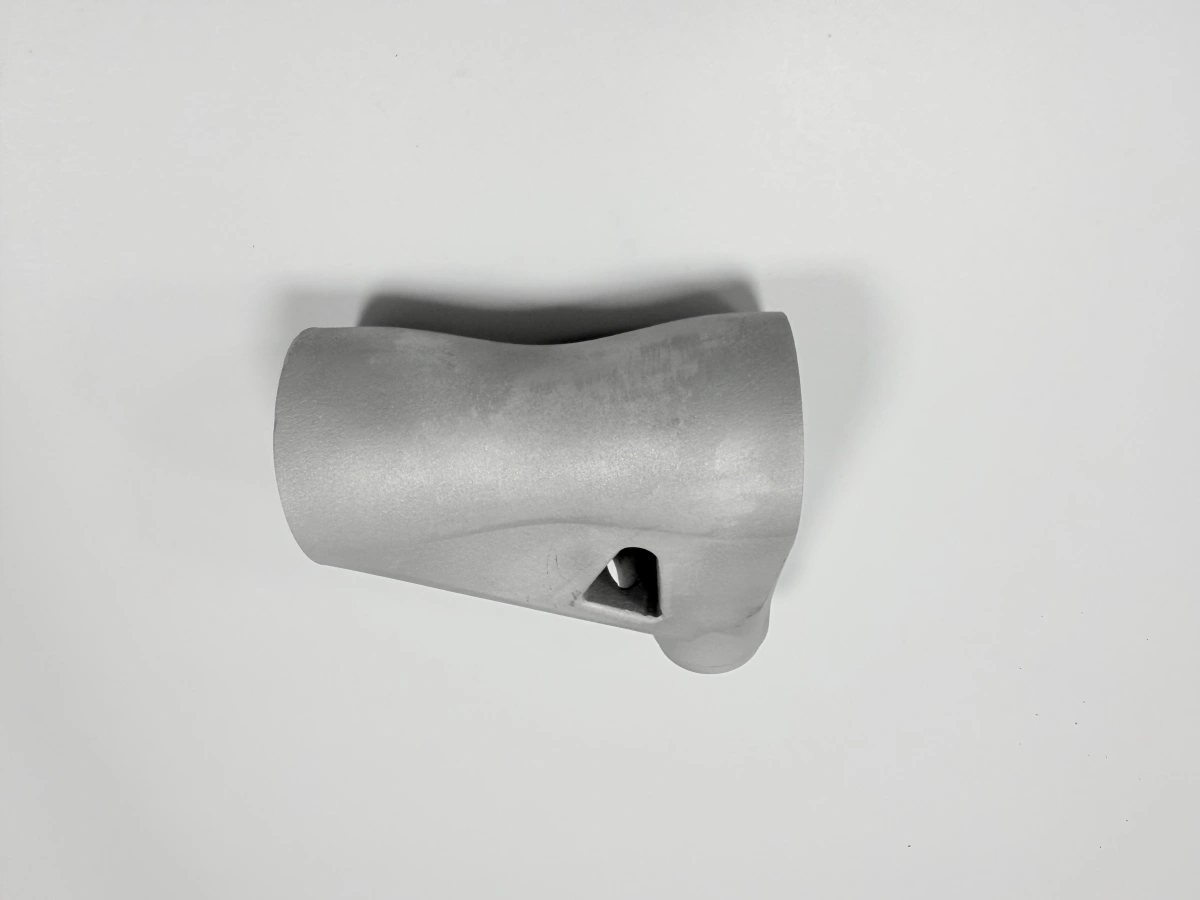
Complex geometry amplifies the distinction. A lattice has thin struts and high surface area; a blind bore has limited access; a conformal channel has changing curvature and section; a sharp internal corner can retain a support mark. Pressure can be uniform in the vessel while thermal response, cleaning, restraint, and inspection are not uniform in the part because a thermal gradient and limited support access change the final material state. The route depends on the feature and the claimed result, so an external roughness reading or bulk density number cannot prove internal surface quality.
Access and Finishing Options
For an open channel, choose cleaning, abrasive flow, blasting, chemical finishing, electropolishing, or another validated route only when it is compatible with the material and feature. For a blind or enclosed passage, assess whether the media can enter and exit, whether residue can be removed, and whether the process changes entrance size or wall thickness. Machining can establish an accessible bore but cannot reach every conformal path. Coating can add protection but introduces thickness, adhesion, and blockage risks. Use the surface-treatment route only with a feature-specific verification plan.
For a 316L conformal-cooling manifold, select HIP when pore-driven leakage or fatigue is the issue and the channels can be cleaned and inspected. Then verify CT or a validated internal method, wall thickness, flow, pressure leak performance, and residue removal. For a tool-steel insert, choose HIP when internal defects threaten channel life, then machine and polish the cavity and inspect datums and channel function. For a lattice bracket, question a polishing claim unless the method can reach the struts without damaging the geometry; verify strut size, surface state, and the service test that matters.
Complex internal surfaces also need a final-state check after any heat treatment, cleaning, or finishing operation. A channel can pass before treatment and fail after residue, distortion, coating thickness, or abrasive accumulation changes its section. Define a cleaning endpoint, inspect the entrance and exit, and use a flow or pressure condition that represents service. If the method cannot observe the internal wall or distinguish a restriction from a leak path, the surface claim remains open and the part should not be released as smooth.
Inspection Limits
Select the inspection method from the internal claim. CT can resolve internal geometry and indications only within its voxel size, contrast, threshold, and access limits. A borescope can show selected visible regions but not a hidden wall. Flow or pressure testing demonstrates a functional response under stated conditions but may miss a local roughness or wall defect. A replica or sectioned metallography can provide local surface evidence but may be destructive. Record method, resolution, location, orientation, uncertainty, sampling, cleaning state, and acceptance criterion.
Use a staged check. Inspect the cleaned part before HIP, capture internal geometry or defect data, record the thermal cycle, and re-inspect after cooling. Perform internal finishing or machining if selected, then repeat the feature-specific inspection. Test flow, pressure, leakage, or thermal performance after the final operation. If CT shows improved porosity but the channel still fails flow or the internal feature cannot be measured, the part remains unresolved. A functional test is evidence for its tested condition, not a blanket certificate for every internal surface.
Size and Geometry Boundary
Large sections can have a different heat-up and cooling history from thin walls. Small lattices can be difficult to clean and measure even when they fit easily in the vessel. Fixtures can stabilize one datum while transferring movement to another. Define the outside envelope, thickest section, thin features, channel diameter, blind depth, minimum wall, support state, fixture, load position, and machining allowance. Use the HIP process only after the vessel and load envelope are qualified for the material and geometry.
Provide CAD and drawing revision, material and lot, additive route, orientation, internal feature map, trapped-material risk, target roughness or functional criterion, HIP cycle, cleaning and finishing route, inspection resolution, flow or leak condition, quantity, and acceptance authority. Request cycle charts, CT or internal inspection, dimensional maps, final surface evidence, cleaning record, functional tests, and deviations. HIP can support internal reliability when its mechanism and evidence fit the defect; it does not establish a smooth internal surface or complex-geometry qualification by itself.
For RFQ preparation, request the HIP processing service after the buyer defines the material state, quantity, and required verification method.
For final release, compare the surface-treatment service with the inspection record, service condition, and disposition of any unresolved risk.
.webp)